A customer sends back a magnet that measured fine when it left the factory. Six months later it will not hold a screwdriver. Nothing about the material changed. Something about the service conditions did. In practice, neodymium magnets lose strength for four reasons, and each one leaves a fingerprint.
Sintered neodymium magnets are stable when they are used inside their limits. When they lose strength in the field, it is almost always one of four causes. Each one leaves a different fingerprint, so you can usually tell which one you have before you spend money on a fix.
Why Neodymium Magnets Lose Strength: A Magnet Rarely Fails on Its Own
Start by separating two kinds of loss. Reversible loss comes back when the magnet cools down or the opposing field is removed. Permanent loss does not come back. Only the second one shows up as a magnet that has genuinely become weaker, and only the second one needs a material change.
Cause 1: Heat Above the Grade’s Limit
This is the most common cause, and the easiest to confirm. Every neodymium grade has a maximum working temperature. Run the magnet above it and the operating point slides down the demagnetization curve until it passes the knee. Once it passes, part of the alignment is lost for good.
The Three Numbers That Decide It
Three figures set the limit, and they are not interchangeable.
| Figure | What it controls |
|---|---|
| Br (remanence) | The flux the material can hold at room temperature. It sets the field at a given distance. It says nothing about heat. |
| Hcj (intrinsic coercivity) | How hard it is to push the material past the knee. This is the number that decides whether the field comes back after a hot day. |
| Maximum working temperature | The highest magnet temperature at which the magnet still holds its working point, at the geometry you are using. |
The Grade Suffix Is the Temperature Rating
In the standard naming, the letter after the number tells you the temperature class. Our normal range for motor and sensor work is N30 to N38AH, and the suffix moves with the duty.
| Grade suffix | Maximum working temperature | Typical use |
|---|---|---|
| N | 80 °C | Room-temperature motors, sensors, holding work |
| M | 100 °C | Small motors with modest duty cycles |
| H | 120 °C | Continuous-duty servo and pump motors |
| SH | 150 °C | Motors in warm enclosures, automotive under-hood |
| UH | 180 °C | Traction motors, hot actuators, wind generators |
| EH | 200 °C | High-temperature industrial and aerospace duty |
| AH | 230 °C | Extreme duty, where samarium cobalt is often the better answer |
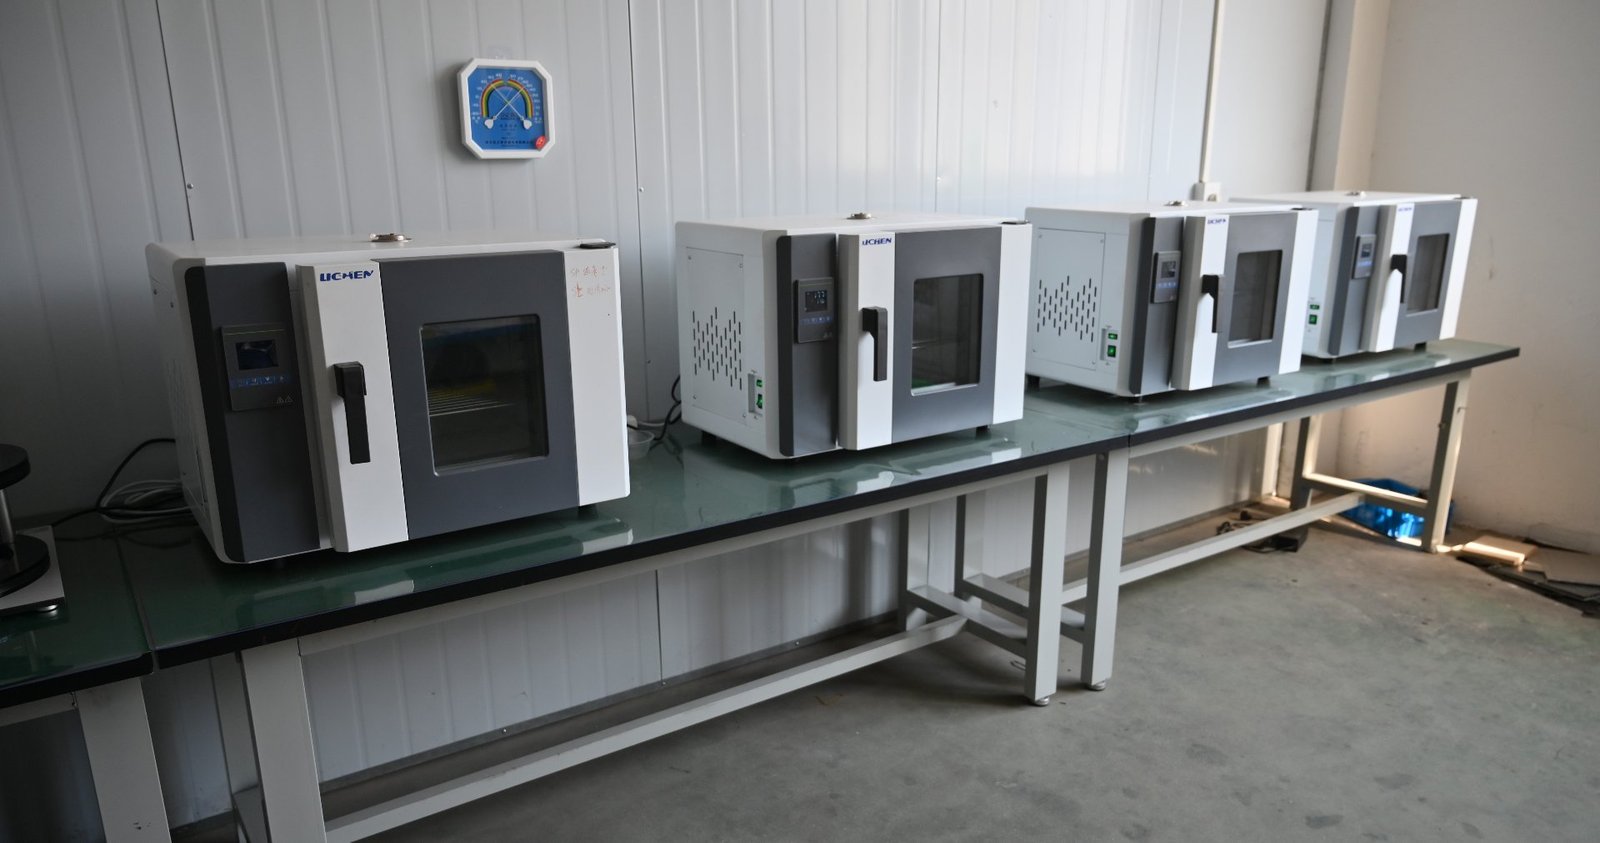
High-temperature ovens are used to measure irreversible loss before a magnet goes into a hot application.
Cause 2: The Coating Failed Before the Magnet Did
Sintered NdFeB is a powder metallurgy product. The grain boundaries corrode readily, especially in humidity or salt air. A magnet that looks intact on the outside can already have a corroded layer under a chipped coating.
Nickel-copper-nickel is the usual choice for motors. Epoxy coatings hold up better in salt spray and in marine air. Zinc is cheap but it sacrifices itself in a salt fog test, and it leaves a white residue when it does.
Where Corrosion Starts
- Cut edges and chamfers, where the coating is thinnest
- Scratches from handling, assembly or shipping
- Pockets where moisture sits, such as a closed steel cup or a bonded joint
- Sharp corners on arc segments, which is why we chamfer them
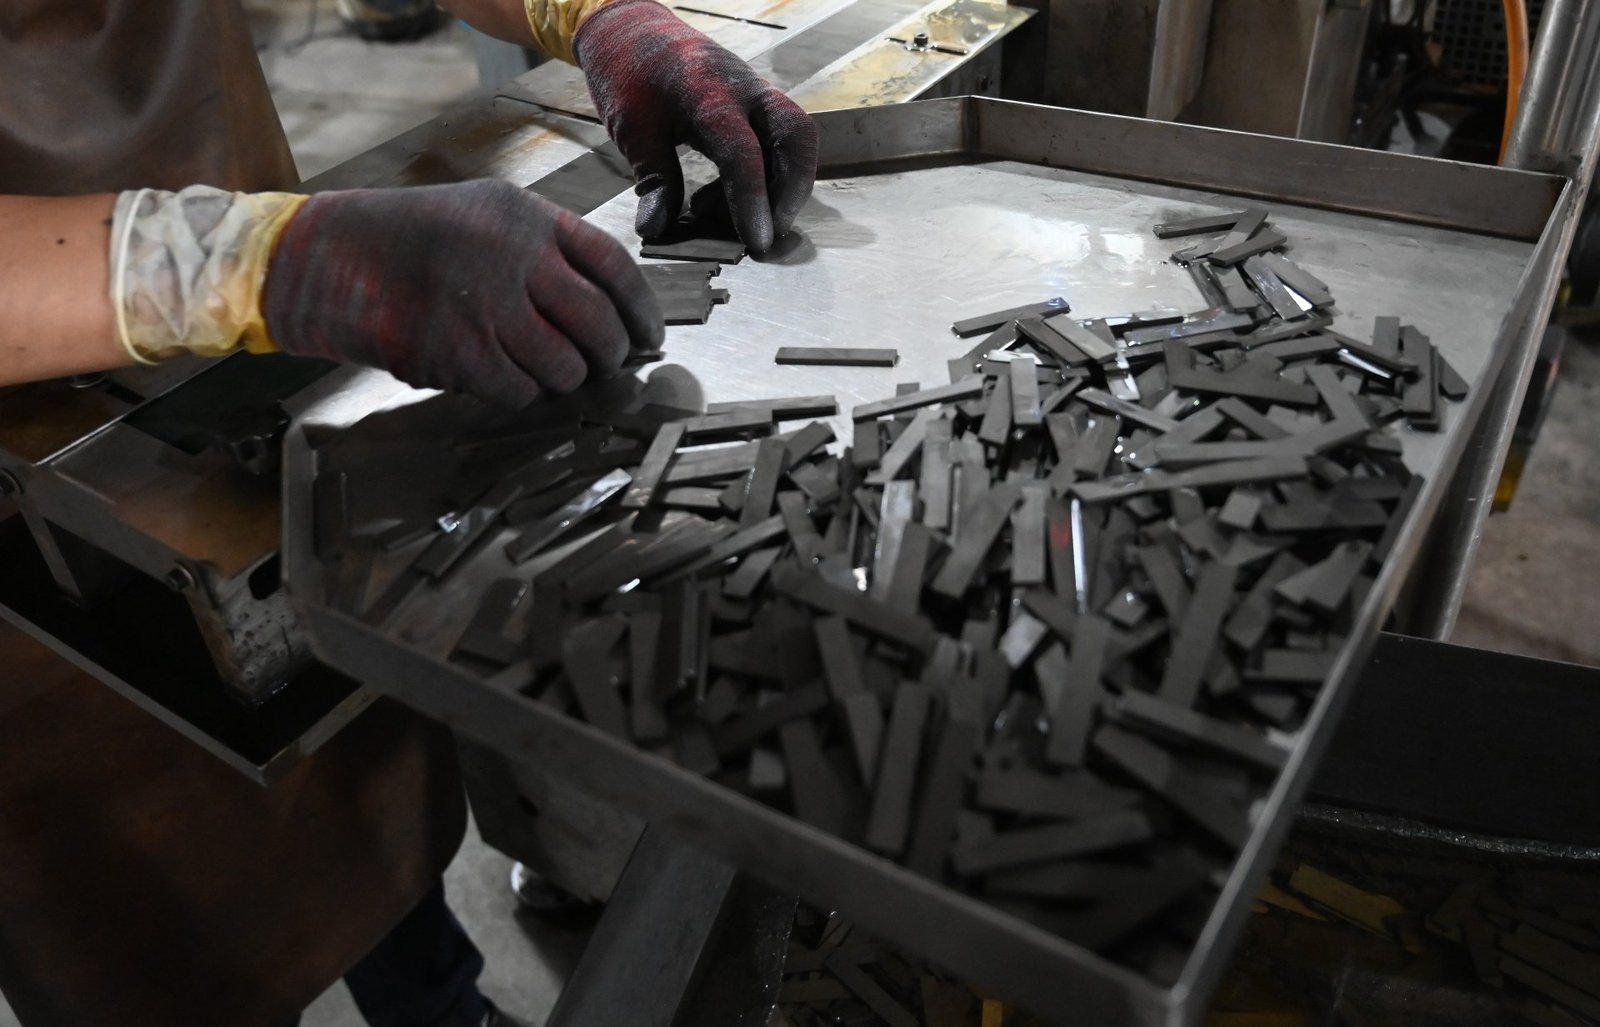
Before chamfering: sharp edges hold a thin coating.
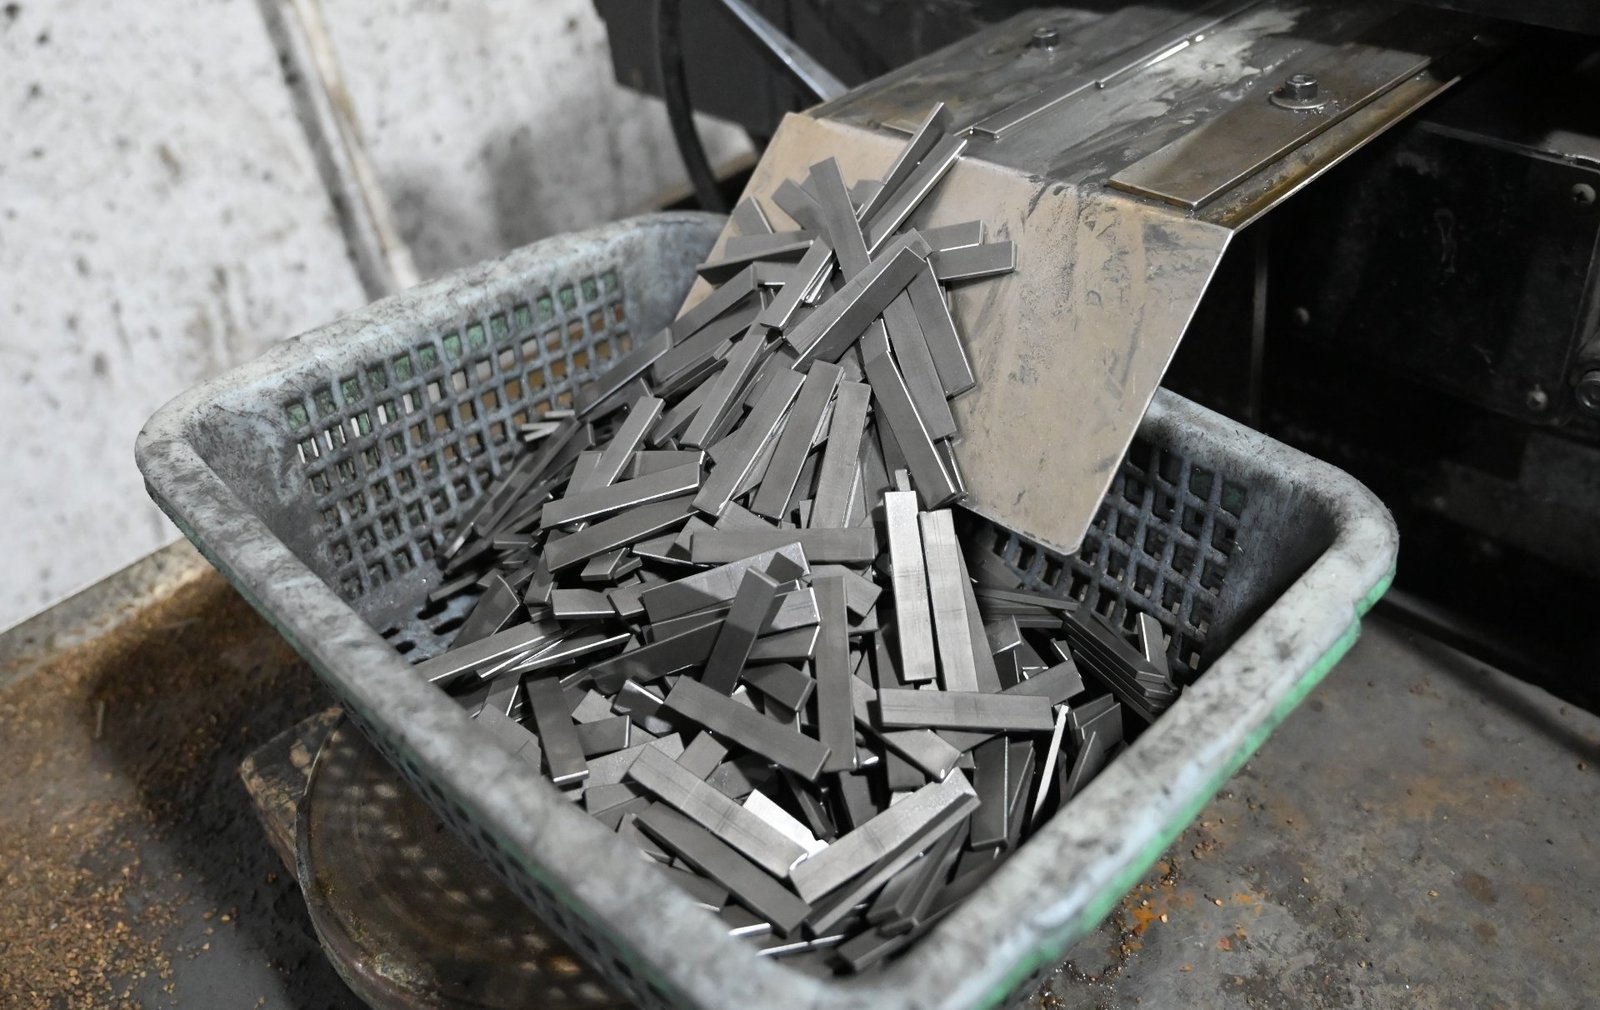
After chamfering: the edge holds coating, so corrosion has fewer places to start.
Cause 3: The Grade Was Chosen on Br Alone
This one is a design mistake, and it shows up months later. A designer compares data sheets, sees that a higher Br gives more flux, and picks the grade with the highest Br. The Hcj column gets less attention.
High Br and high Hcj pull against each other in the same material. Squeeze more flux out of a grade and it usually becomes easier to demagnetize. A grade with a very high Br but a modest Hcj works well on a bench and fails in a hot motor.
Why Hcj Is the Number That Decides
Hcj is the field the material can survive. Anything that pushes the working point left, meaning heat, an opposing field from stator current, or a small air gap, is measured against Hcj. If Hcj has margin, heat only causes reversible loss, and the field returns. If it does not, the loss is permanent.
When you cannot add grade, change the geometry instead. A thicker magnet in the direction of magnetization increases the permeance coefficient, which moves the working point away from the knee. The magnet gets more expensive, but the material stays.
Cause 4: Damage During Assembly
Neodymium is brittle. It is not a structural part, and it should not carry a load. Two magnets that snap together across a gap can chip at the edges. A press fit that needs force can crack a segment. A curved part clamped unevenly can crack along the arc.
The damage itself removes material, but the bigger problem is what follows. A crack exposes uncoated material, and corrosion starts there. That is why a failed magnet often shows two causes at once.
How to Tell Which One You Have
Look at the failed part first. The appearance usually points to the cause.
| What you see | Most likely cause | First thing to check |
|---|---|---|
| Uniform loss, no visible damage, part runs hot | Heat | Measured magnet temperature at the hottest point of the duty cycle, not the ambient |
| Rust, blistering, white or black deposits | Coating failure and corrosion | Coating type against the humidity and salt exposure of the application |
| Loss that started after a design change, cool part | Grade chosen on Br alone | The Hcj margin at the highest expected temperature and opposing field |
| Chips, cracks, or loss near an edge | Assembly damage | Whether the magnet is loaded structurally, and how it is handled before bonding |
| Loss on one pole only, or uneven across poles | Magnetization or handling | The magnetizing fixture, and whether partly magnetized parts were stored loose |
Five Questions Before You Change the Grade
- What is the highest temperature the magnet itself reaches, measured, not assumed?
- What opposing field does the stator or coil apply at that temperature?
- How close does the working point sit to the knee, at that temperature and that field?
- What coating is on the failed part, and what is it exposed to?
- Was the magnet loaded mechanically anywhere in the assembly?
Answer those five and the cause is usually clear. Changing the grade before answering them is how a second batch fails the same way.
Frequently Asked Questions
How much loss is normal after a hot cycle?
A small irreversible loss on the first hot excursion is normal, and it settles after that as the part finds its working point. Loss that keeps growing with every cycle, or loss that appears after months at a steady temperature, points to a different cause.
Does dropping or handling a magnet weaken it?
Mechanical shock does not change the magnetisation, so the field comes back unchanged if the part is intact. What a drop does is chip the coating and crack the edges, and corrosion starts at that damage. After a drop, inspect the edges rather than re-measuring the flux.
How do you measure irreversible loss?
We measure the flux of a sample, hold it above its service temperature for a set time, cool it back to room temperature and measure again. The difference between the two readings is the irreversible loss. It takes a flux meter and an oven, and it is the only way to get the number for your part instead of for the grade.
Send Us the Failed Part Details
Tell us the grade you use today, the highest temperature the magnet sees, the coating, and how the part is held in the assembly. Our engineers will come back with the working point, the margin to the knee, and whether the answer is a higher Hcj grade, a thicker section, or a different coating.
Send Your Details