Inside the Workshop
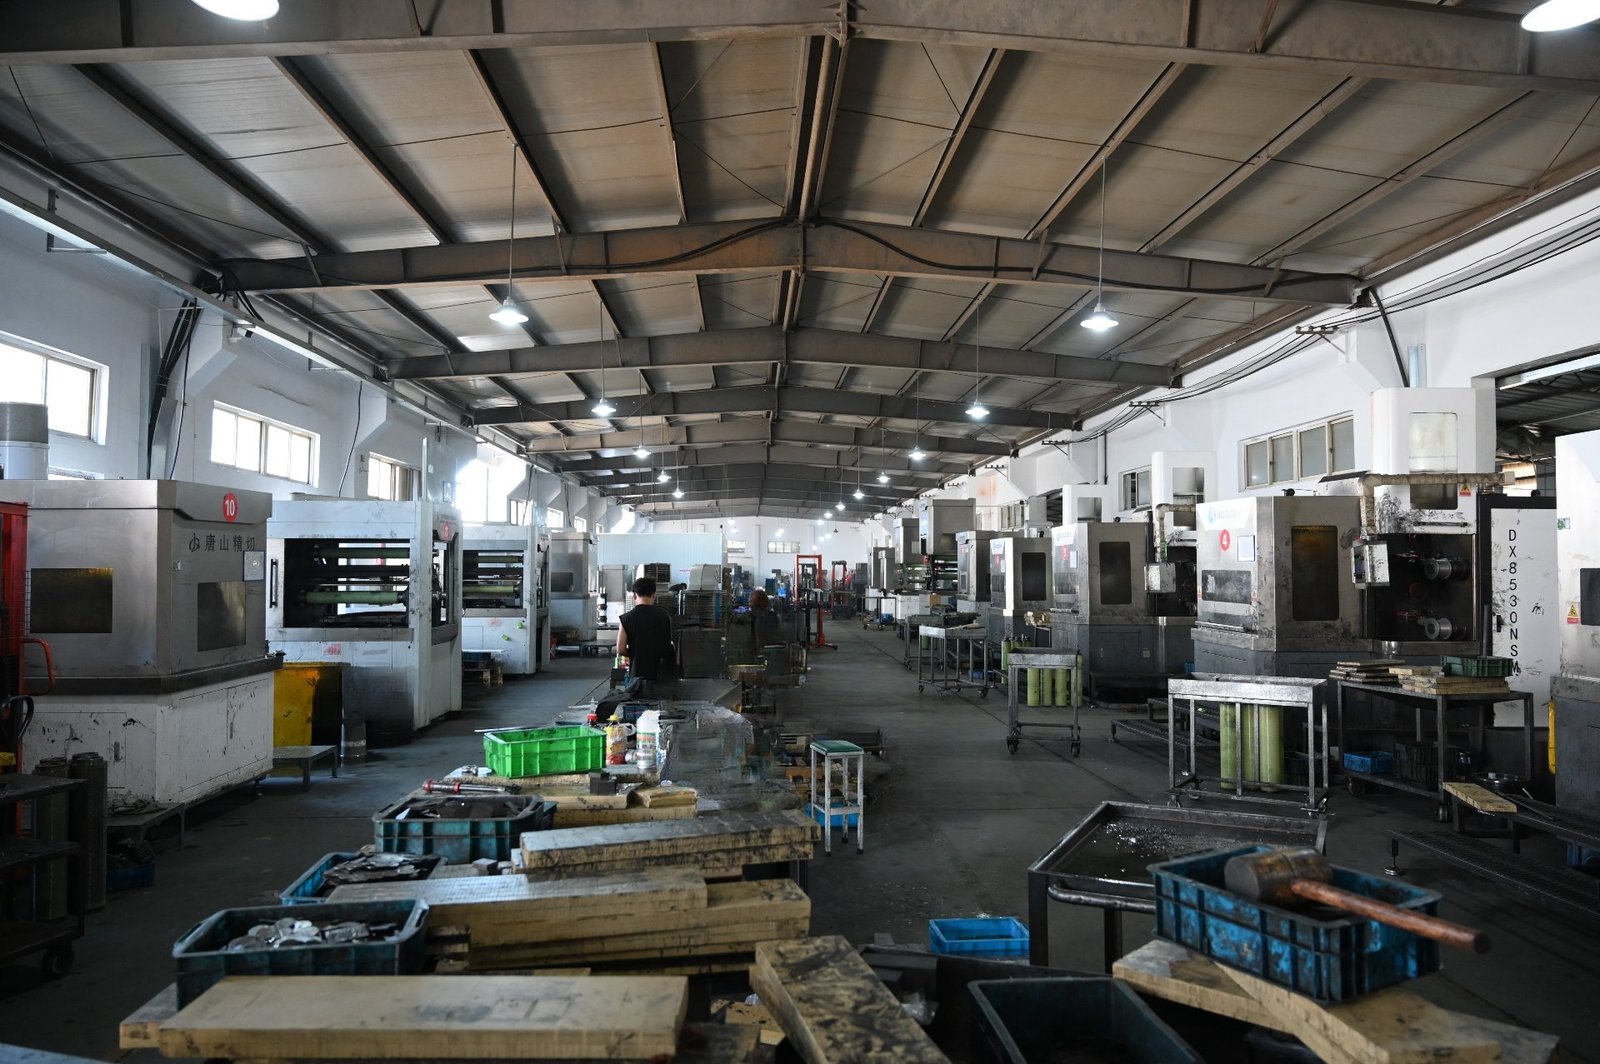
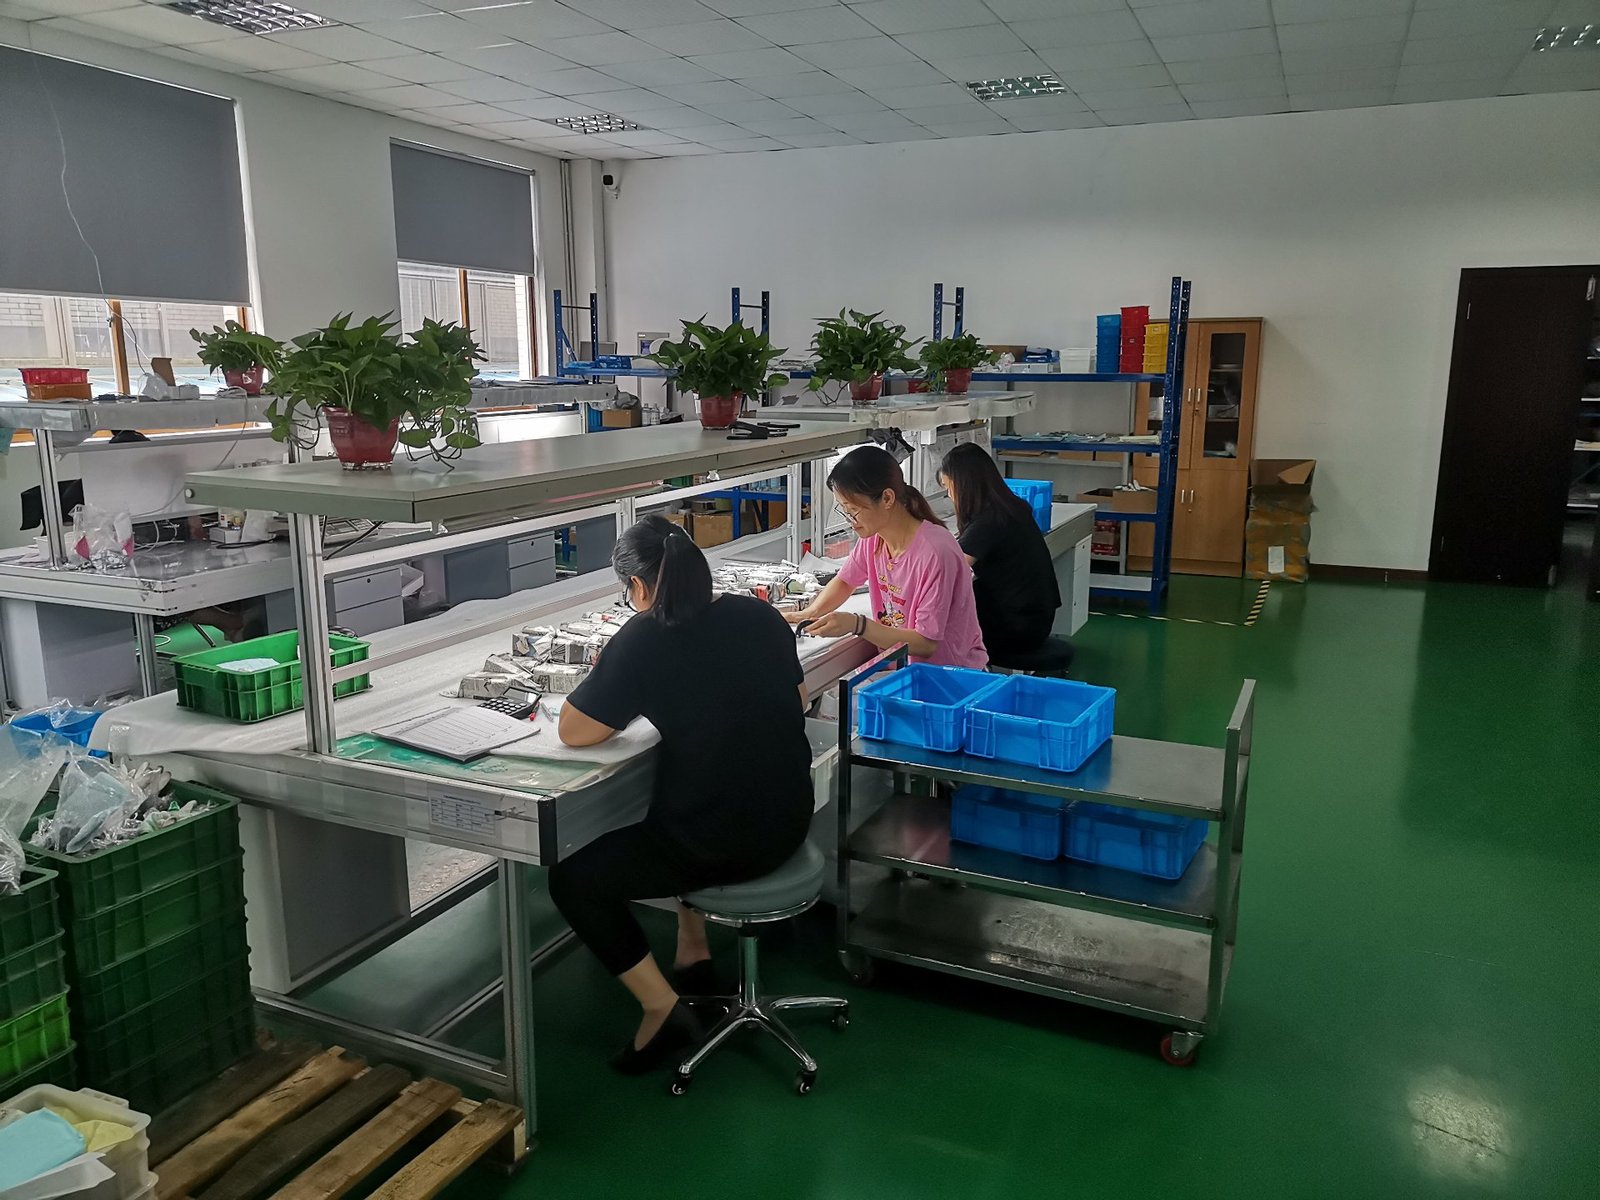
Cutting, finishing, coating, magnetisation and inspection all run under one roof in our neodymium magnet factory. The blank comes from a partner factory. Everything after the blank is ours, which means one team owns the tolerance you receive.
Equipment in Our Neodymium Magnet Factory
These are the machines we run, stage by stage.
| Stage | Equipment | Units | What it does |
|---|---|---|---|
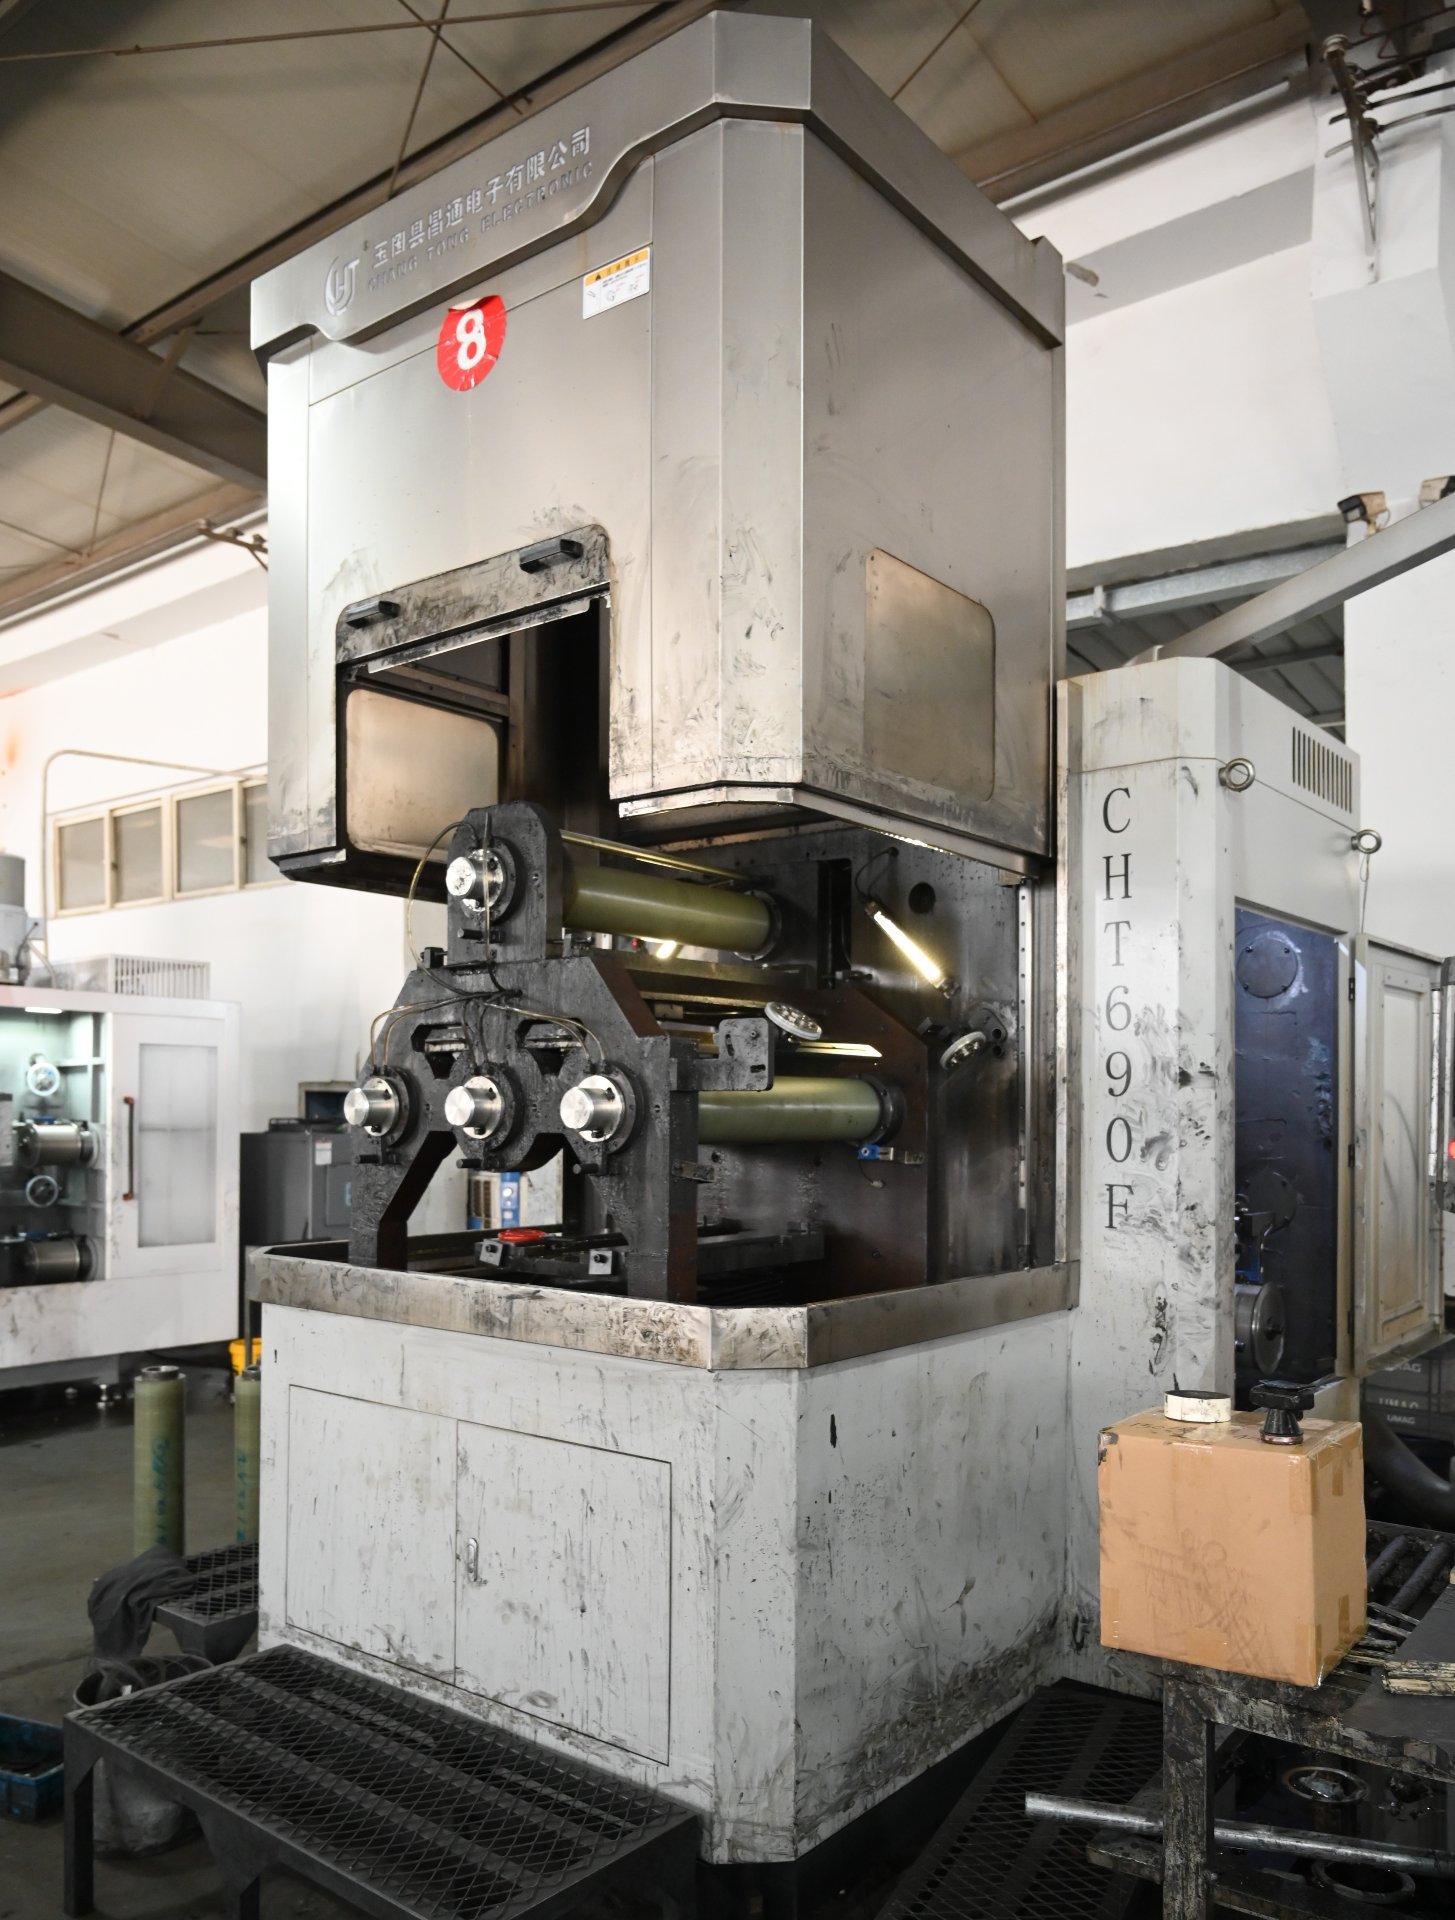
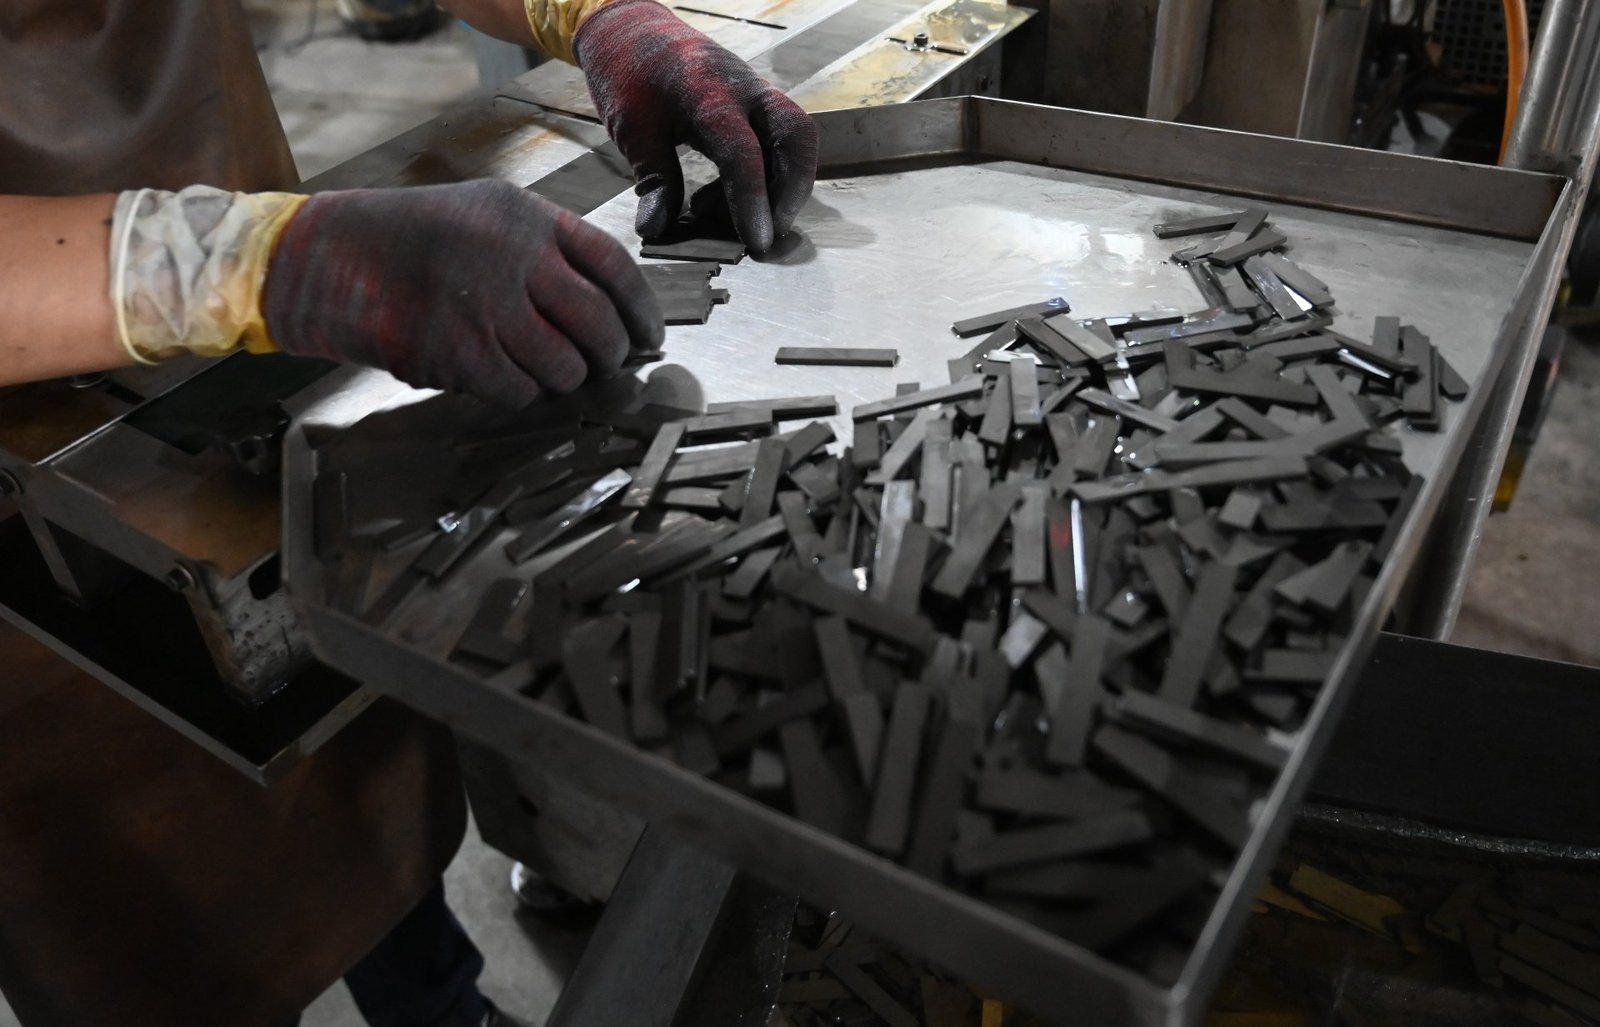
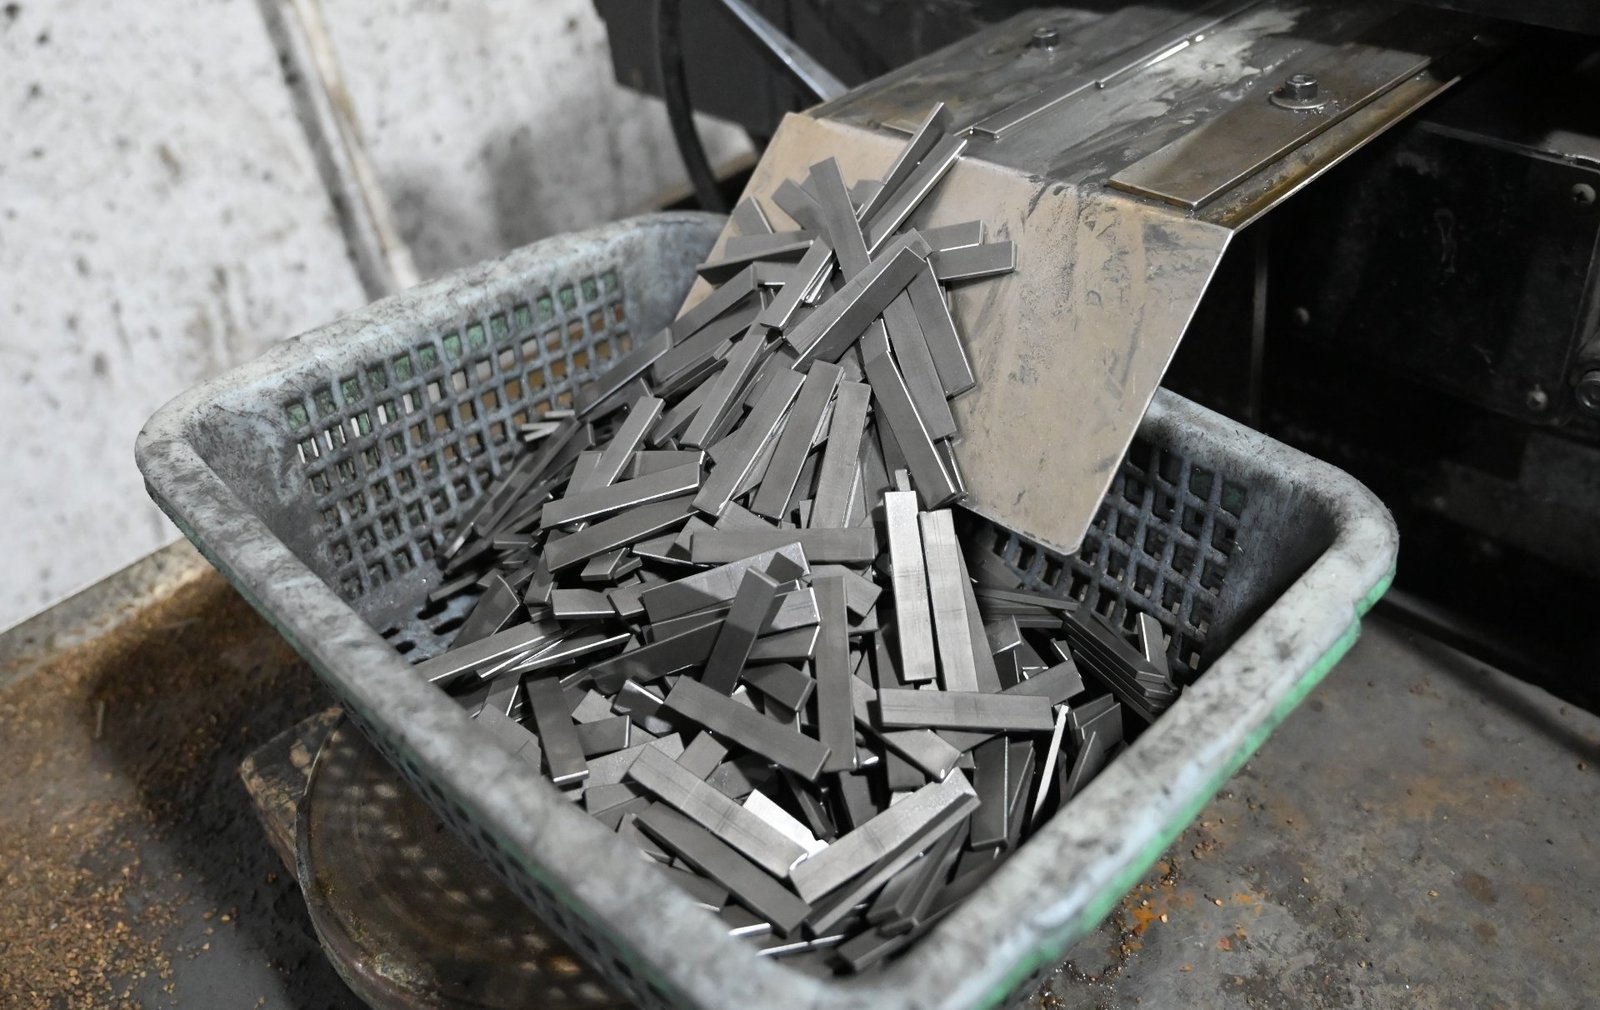
| Slicing | Multi-wire saw | 25 | Cuts blanks into discs, blocks, rings and arcs. About 1 tonne per day in total. |
| Slicing | Small multi-wire saw | 2 | Kept free for samples and prototypes, so they never queue behind production. |
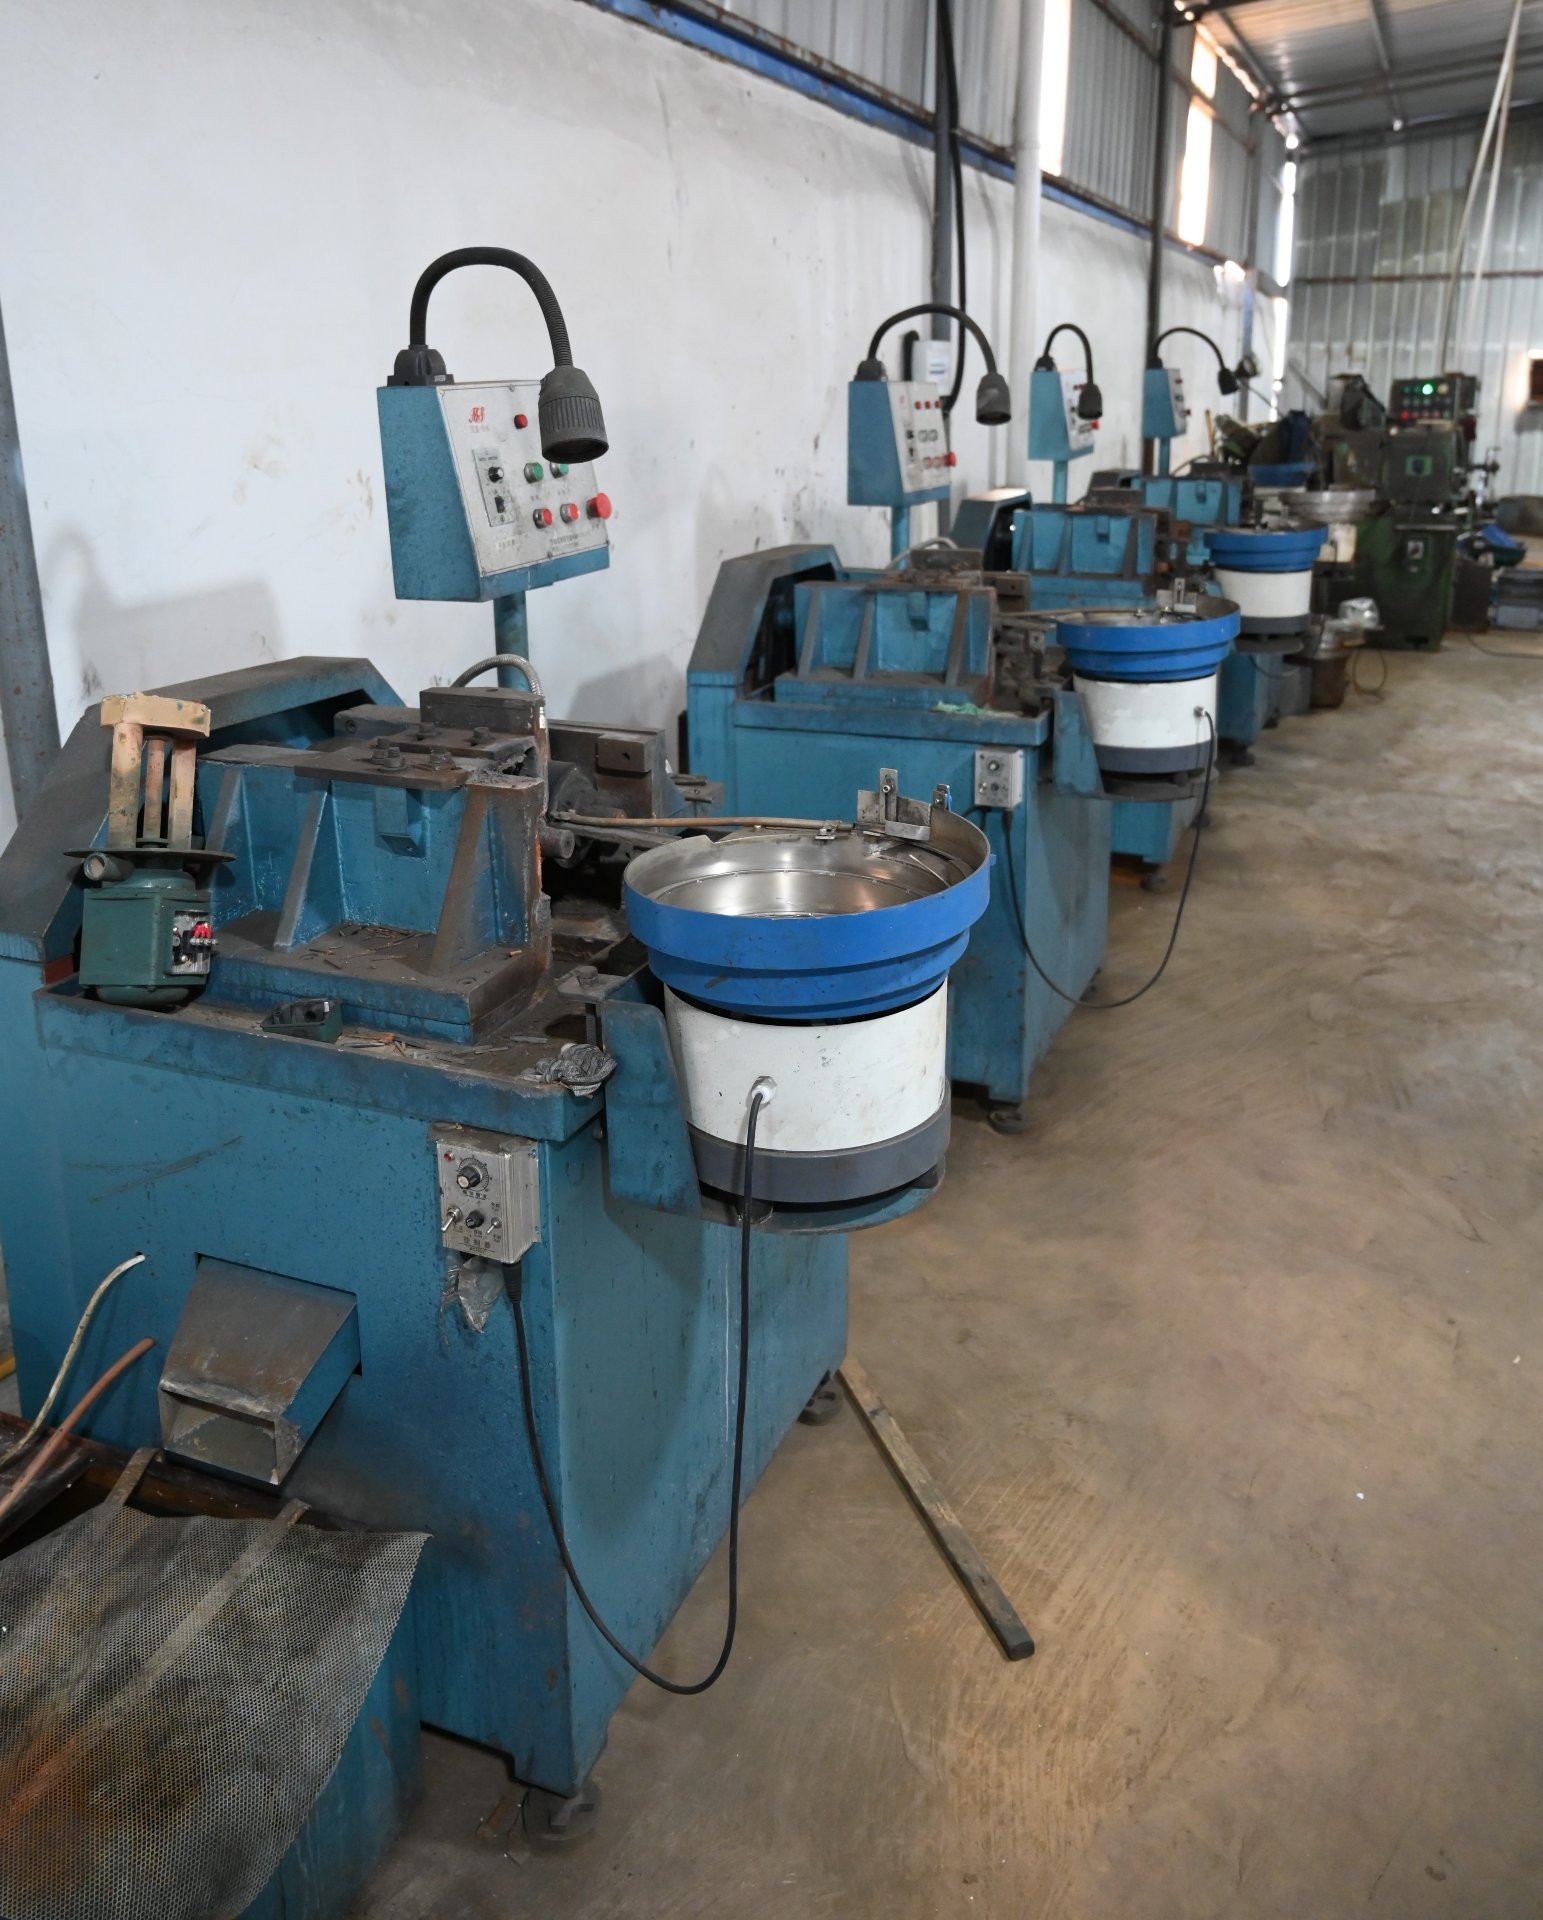
| Chamfering | Chamfering machine | 8 | Breaks sharp edges on flat faces and corners. |
| Chamfering | Tumbling machine | 10 | Rounds edges in bulk. |
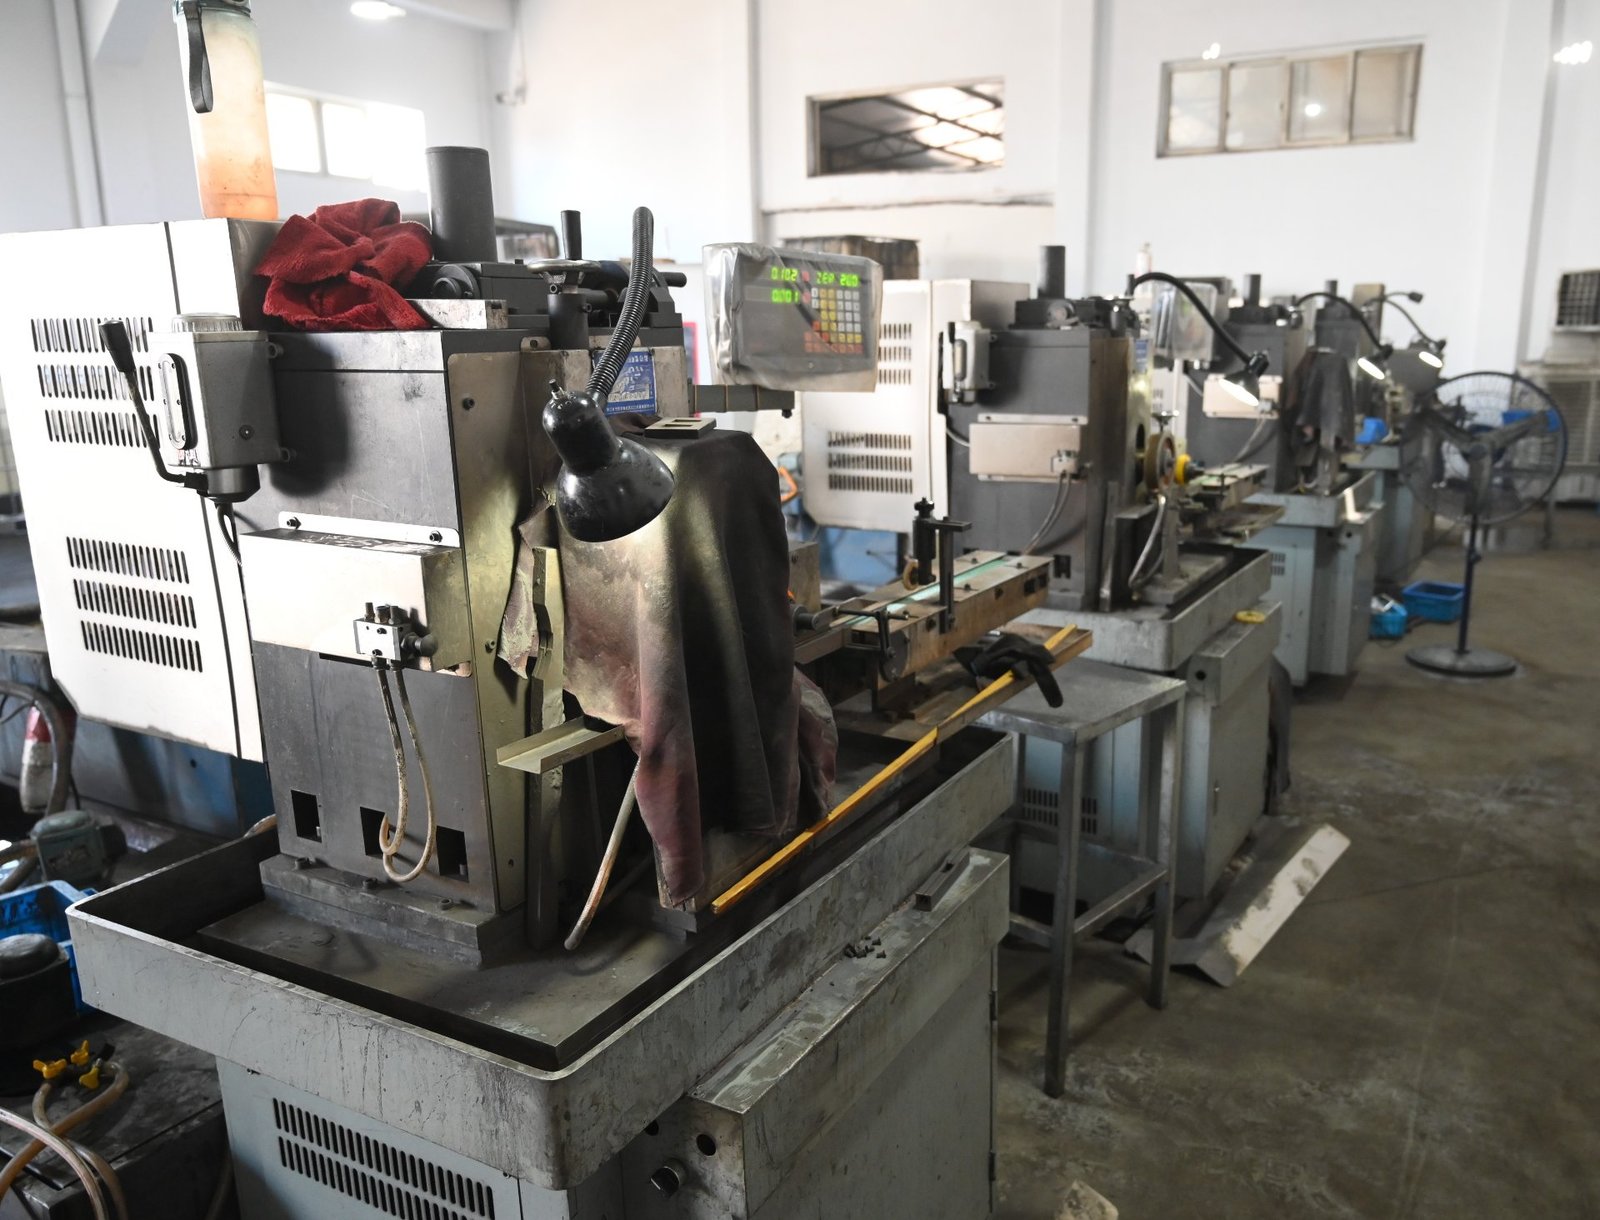
| Grinding | Double-side grinder | 4 | Grinds both faces at once to hold thickness and parallelism. |
| Profile cutting | Arc and tile cutting machine | 18 | Cuts curved segments to the radius on your drawing. |
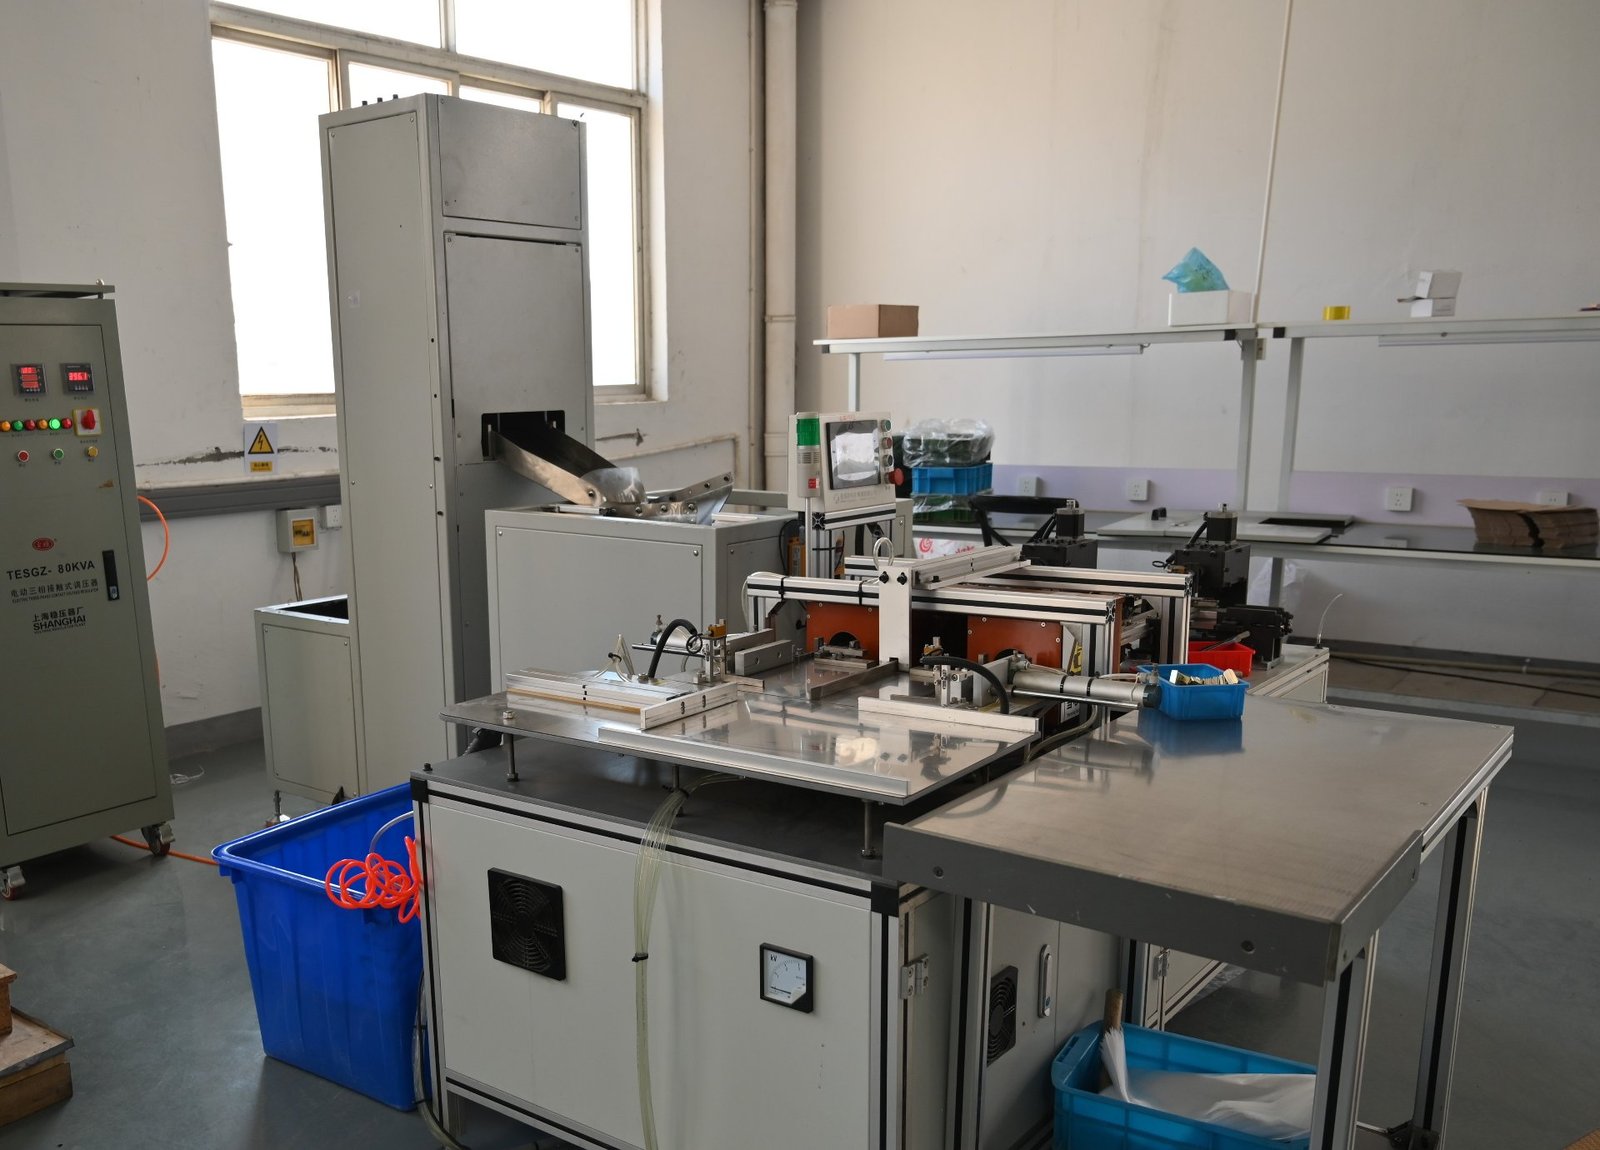
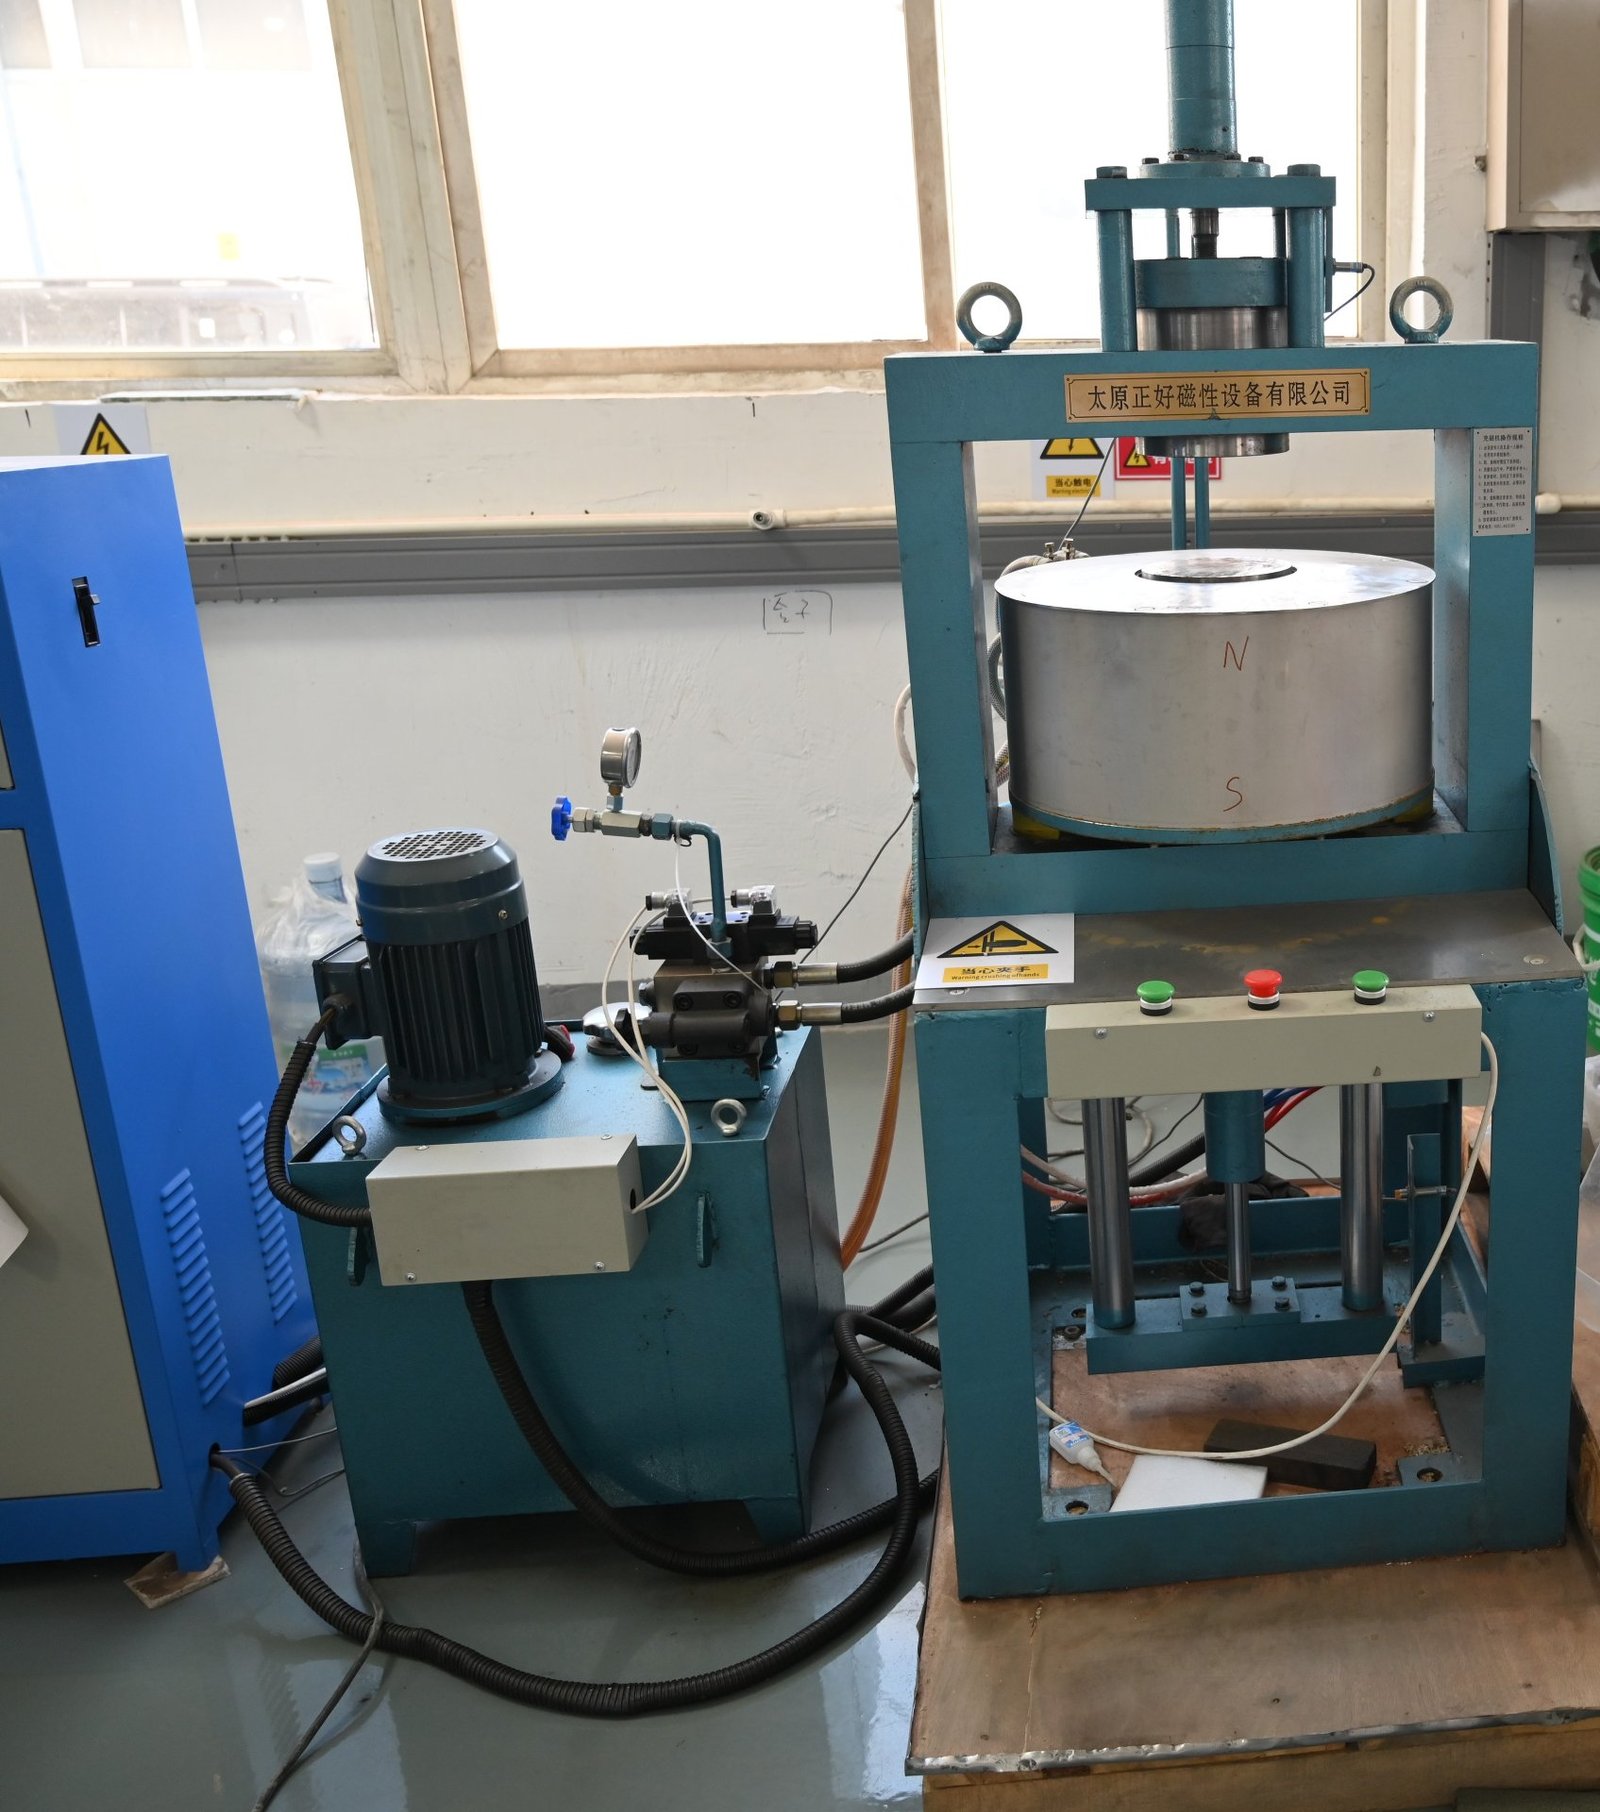
| Magnetisation | Automatic magnetiser | 1 | Volume production with repeatable pole position. |
| Magnetisation | Magnetiser | 4 | General production. |
| Magnetisation | Loose-piece magnetiser | 1 | Single parts and shapes that do not fit a fixture. |
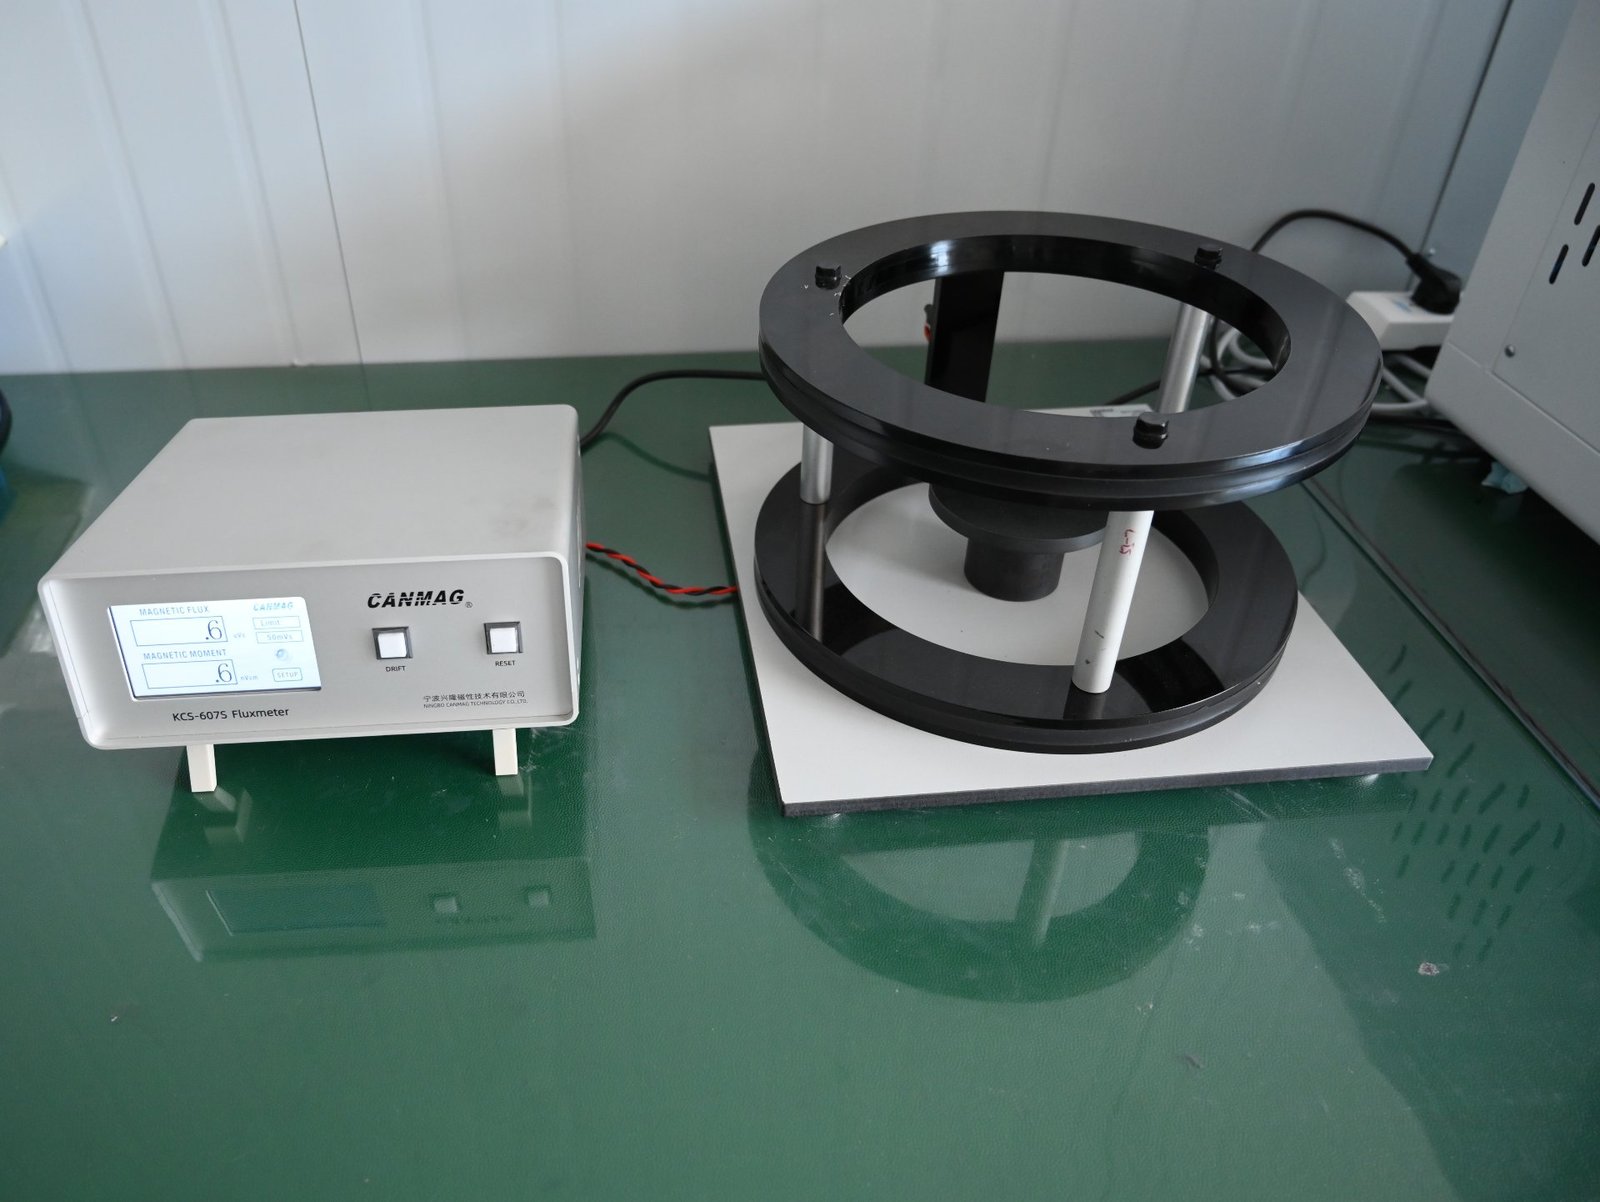
| Inspection | Flux meter | 1 | Magnetic flux on a batch. |
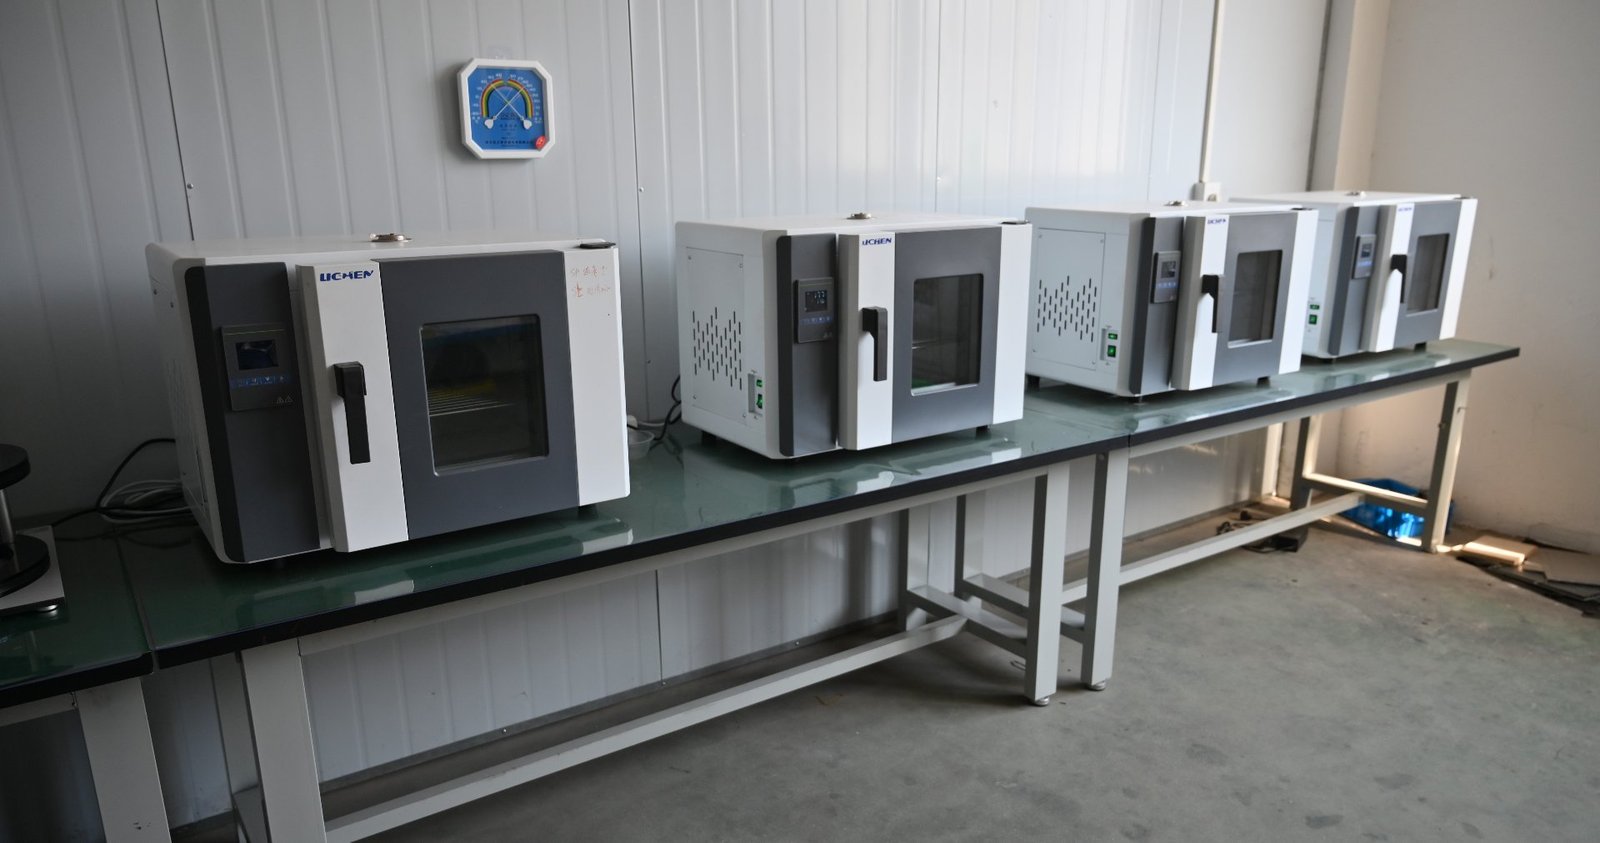
| Inspection | Aging oven | 4 | High-temperature aging and demagnetisation testing. |
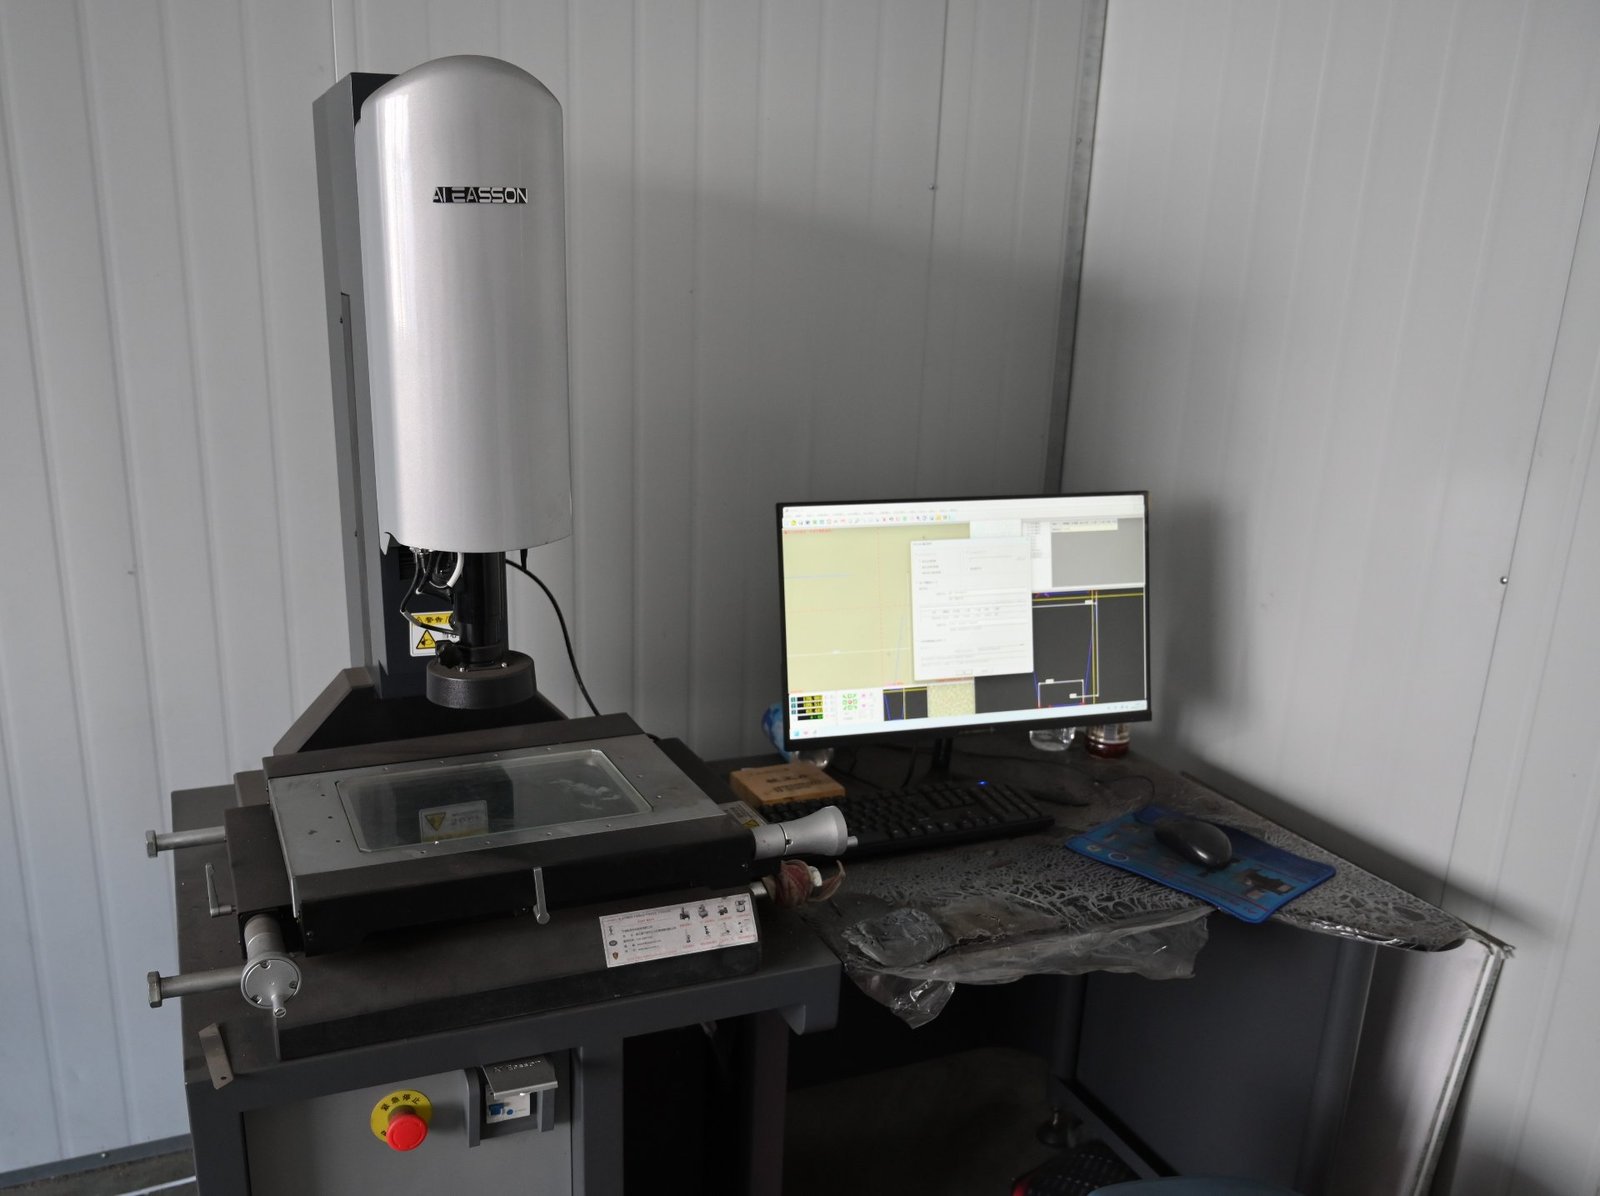
| Inspection | Vision measuring machine | 1 | Dimensions and geometry. |
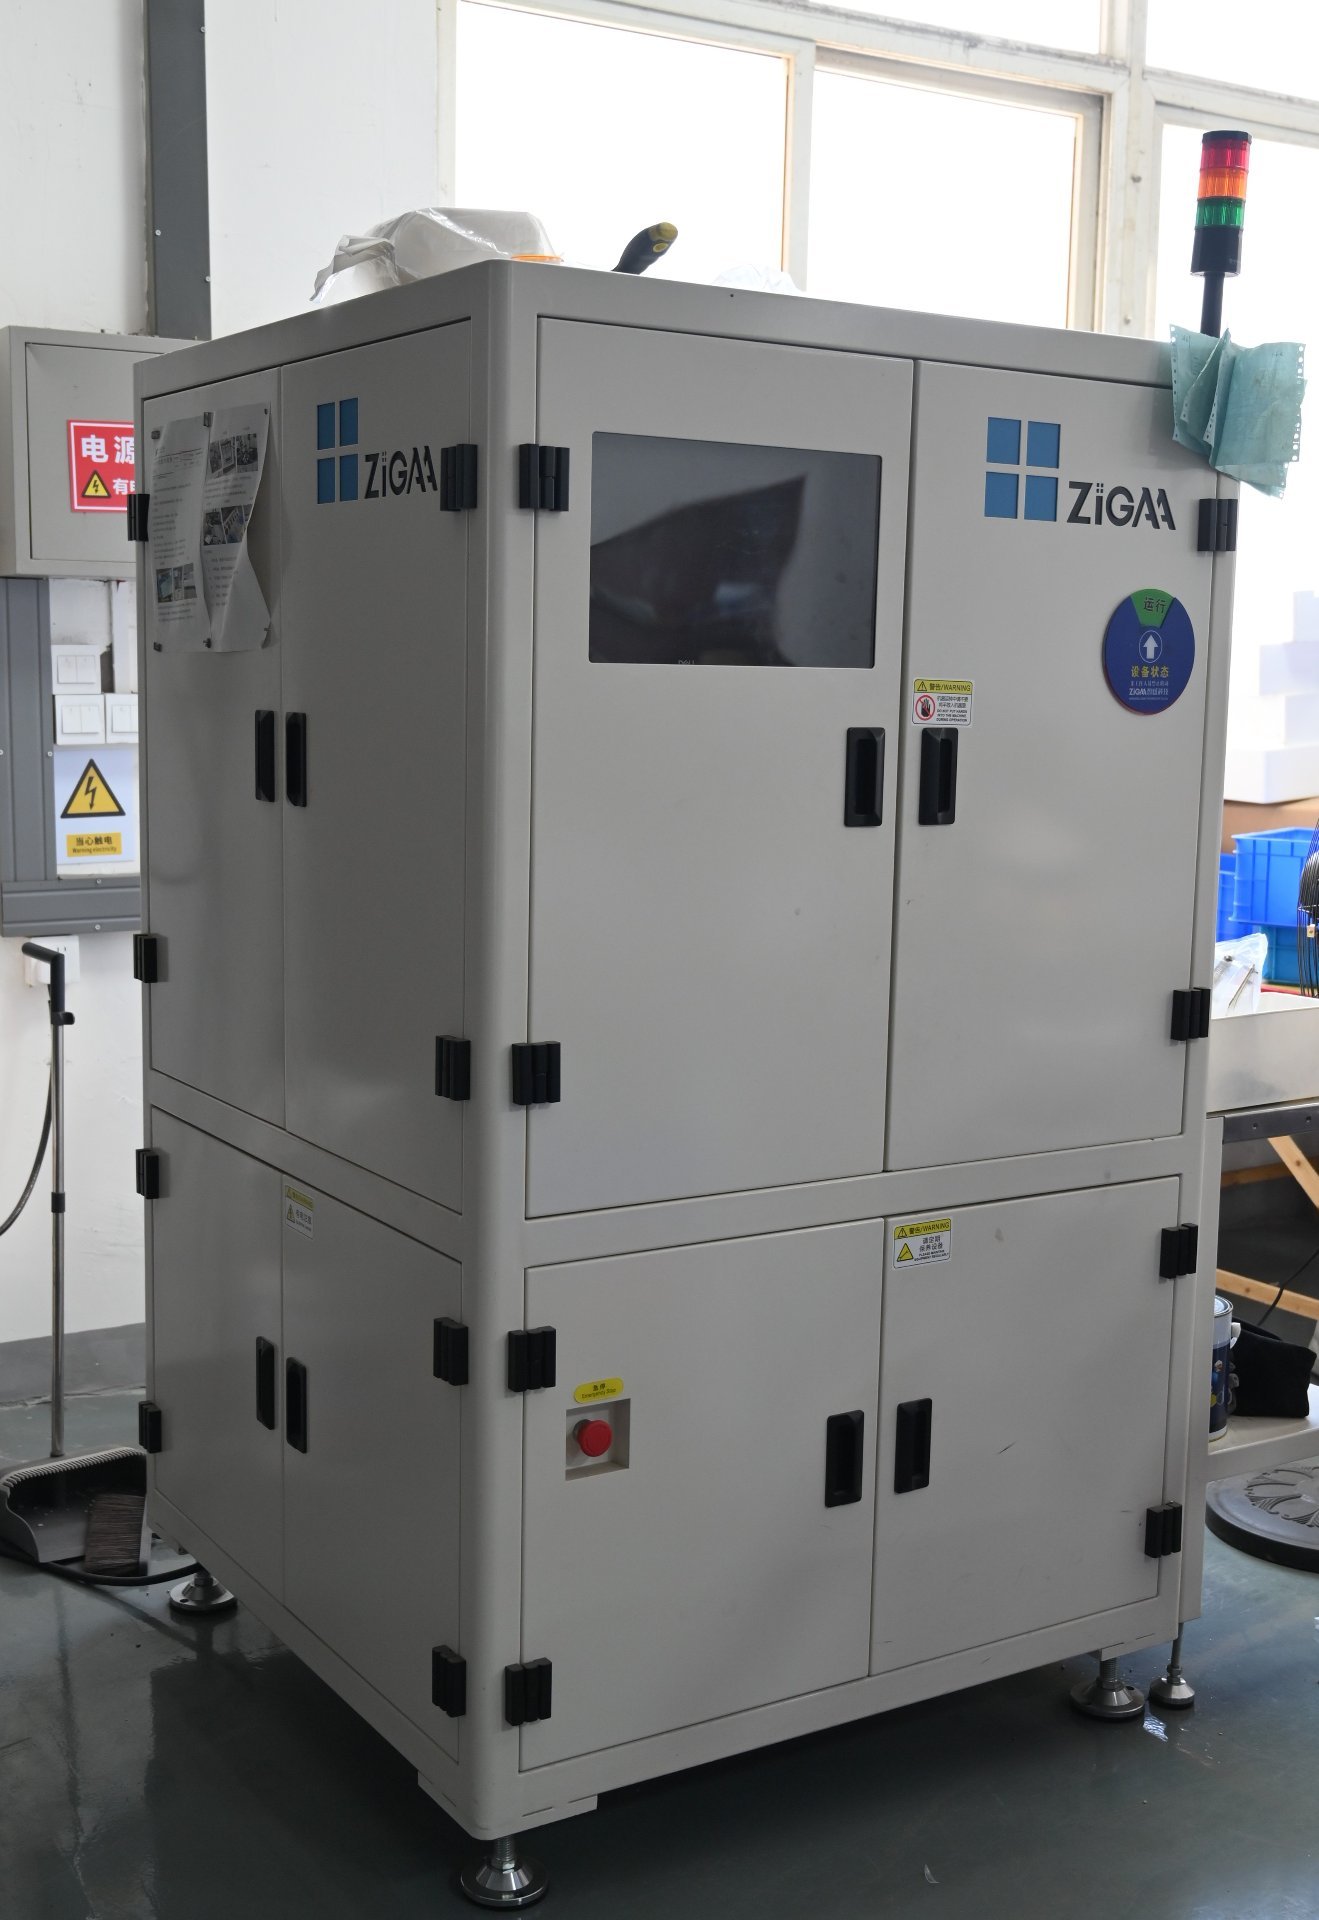
| Inspection | Automated optical inspection | 1 | Chipped corners and surface defects. |
Slicing and Forming
A blank arrives as a sintered block. Slicing decides how many parts come out of it and how much material is lost to the saw. Chamfering and profile cutting decide whether the edges survive coating and whether the curve matches your drawing.
Thickness and Parallelism
Thickness is the dimension that quietly decides motor performance. A few microns of taper across a face changes the air gap, and the air gap changes torque ripple. We grind both faces at the same time, which keeps the two sides parallel to each other.
Chamfering
Slicing leaves sharp edges on every part. Chamfering and tumbling round those edges before coating, so the plating grips the corners instead of chipping off.
Inspection Equipment
What we can measure decides what we can promise. These four instruments cover magnetic, thermal and dimensional checks.
| Equipment | Measures |
|---|---|
| Flux meter | Magnetic flux of a batch, compared against the agreed value. |
| Aging oven (4 units) | Behaviour after time at high temperature, so we can see demagnetisation risk before shipment. |
| Vision measuring machine | Dimensional and geometric features, including flatness, parallelism and concentricity. |
| Automated optical inspection | Chipped corners, edge damage and surface defects, checked automatically rather than by eye. |
Magnetisation
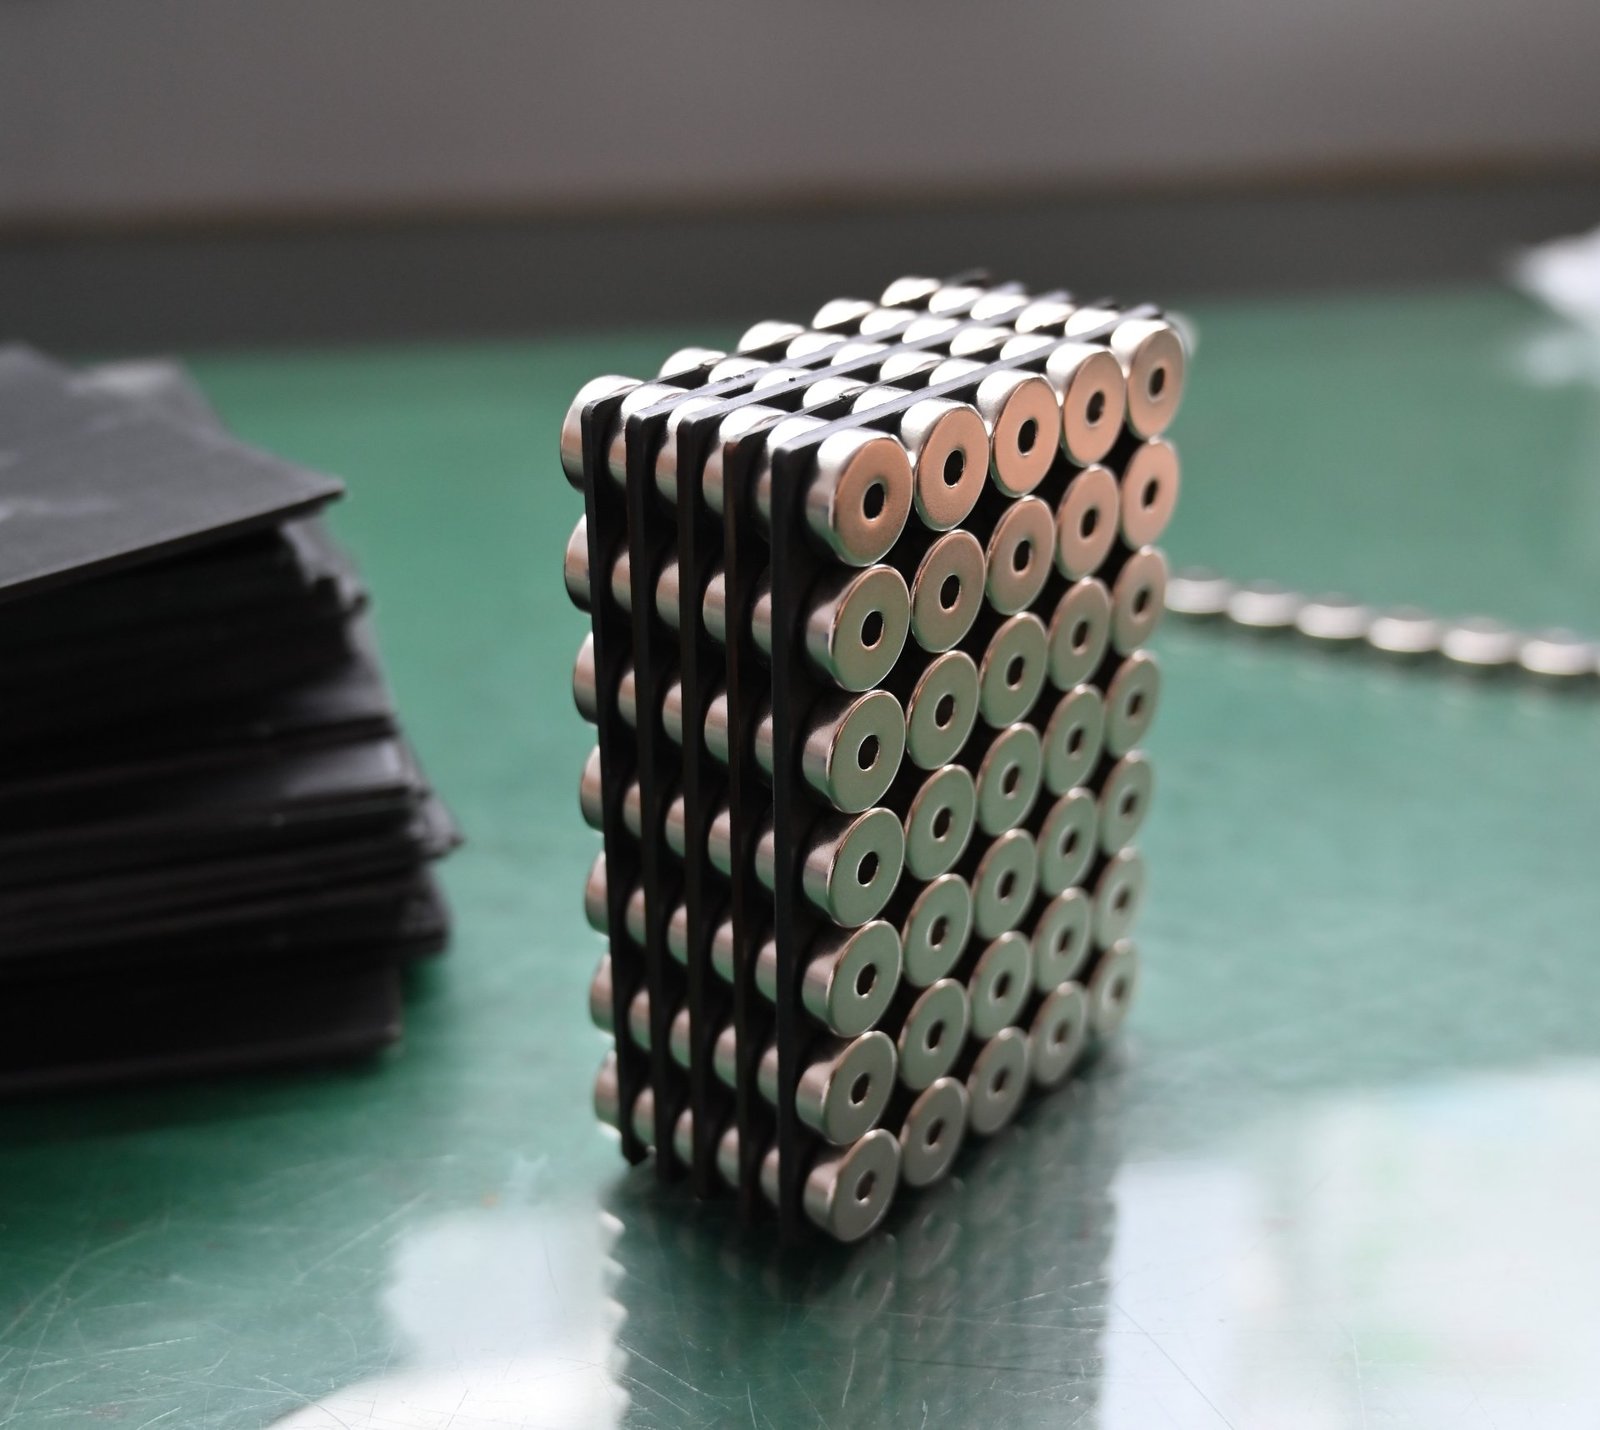
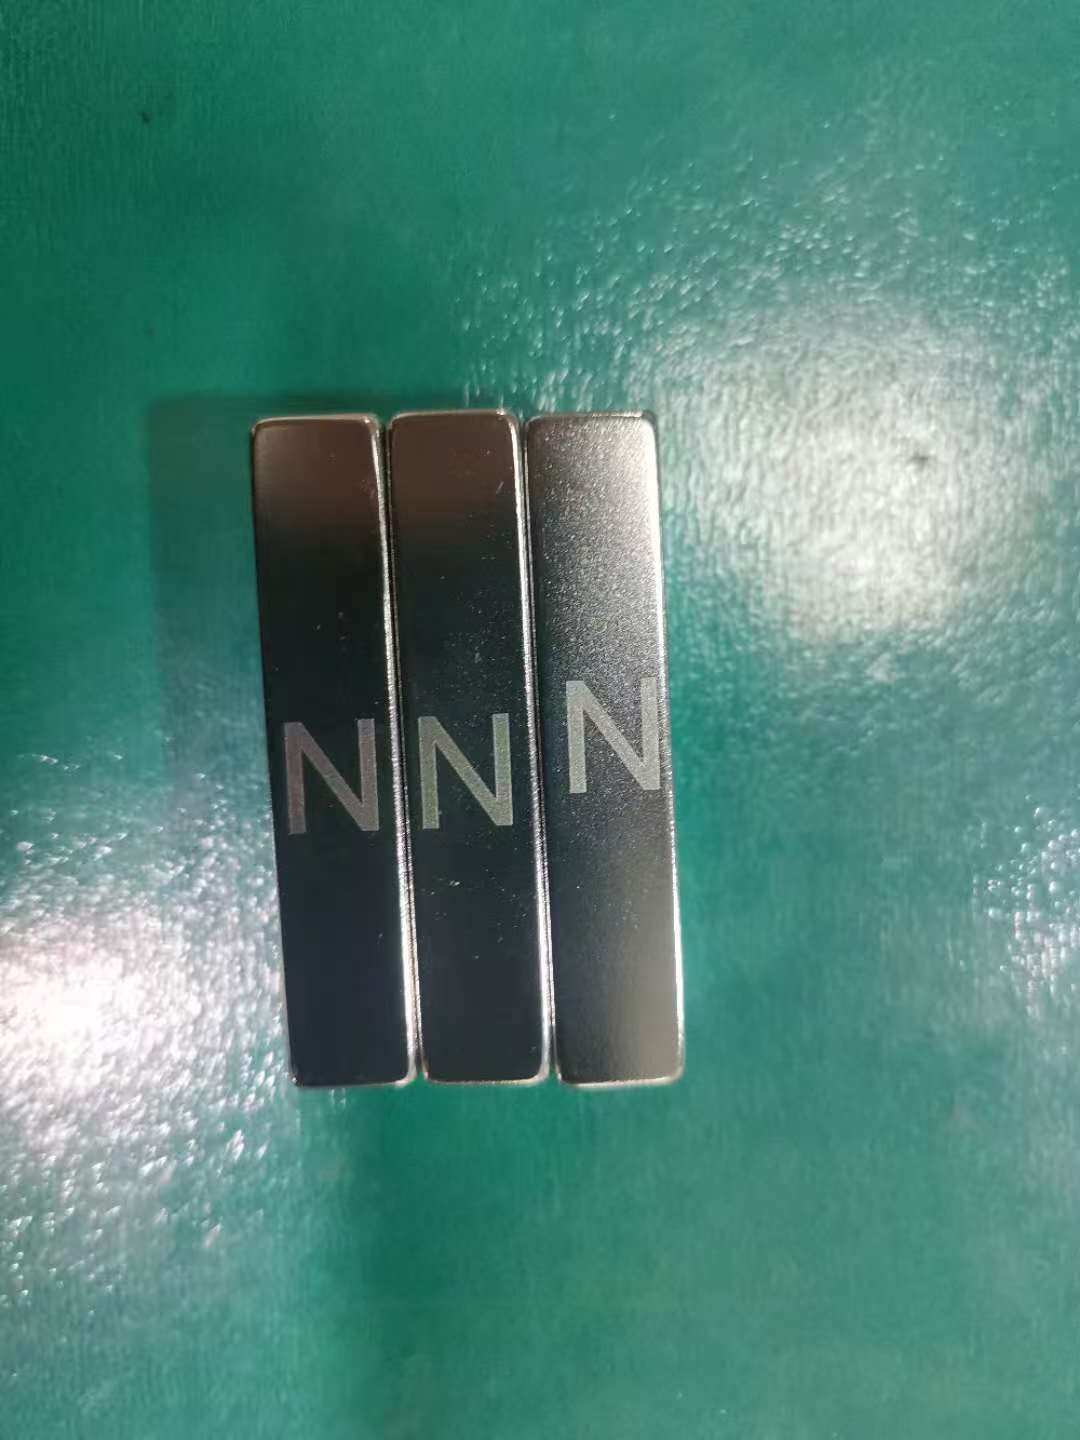
Magnetisation is the last physical step before packing, and it is the one buyers notice first if it goes wrong. Direction, pole pattern and pole position are all set here. A loose-piece magnetiser handles single parts and shapes that will not sit in a fixture.
Packing and Storage
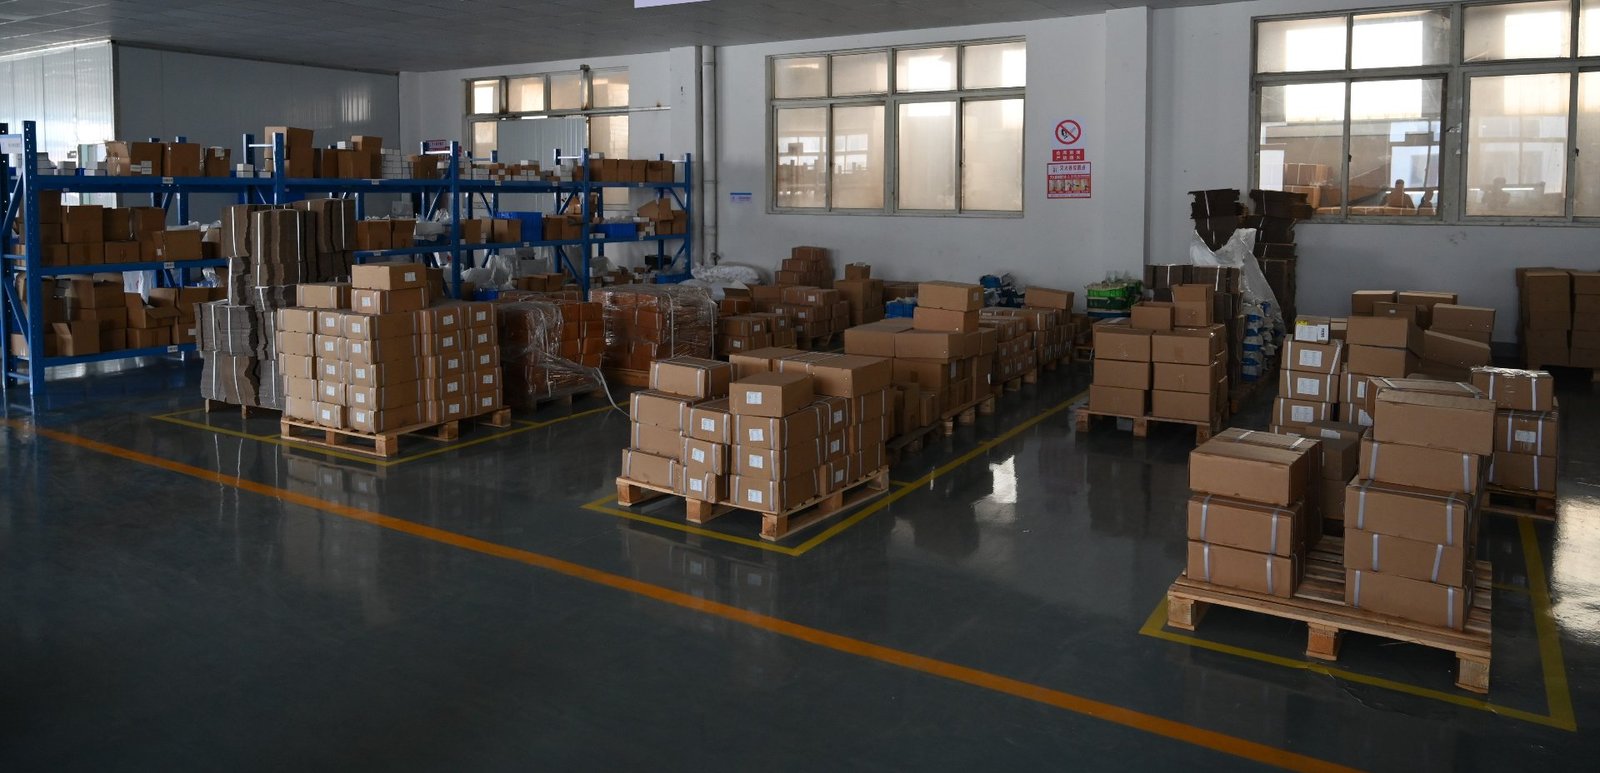
Finished parts are packed in cartons that suit your handling and shipping route. Magnets attract each other in transit, so pack quantity, shielding and carton strength are agreed before shipment.
Blank Production
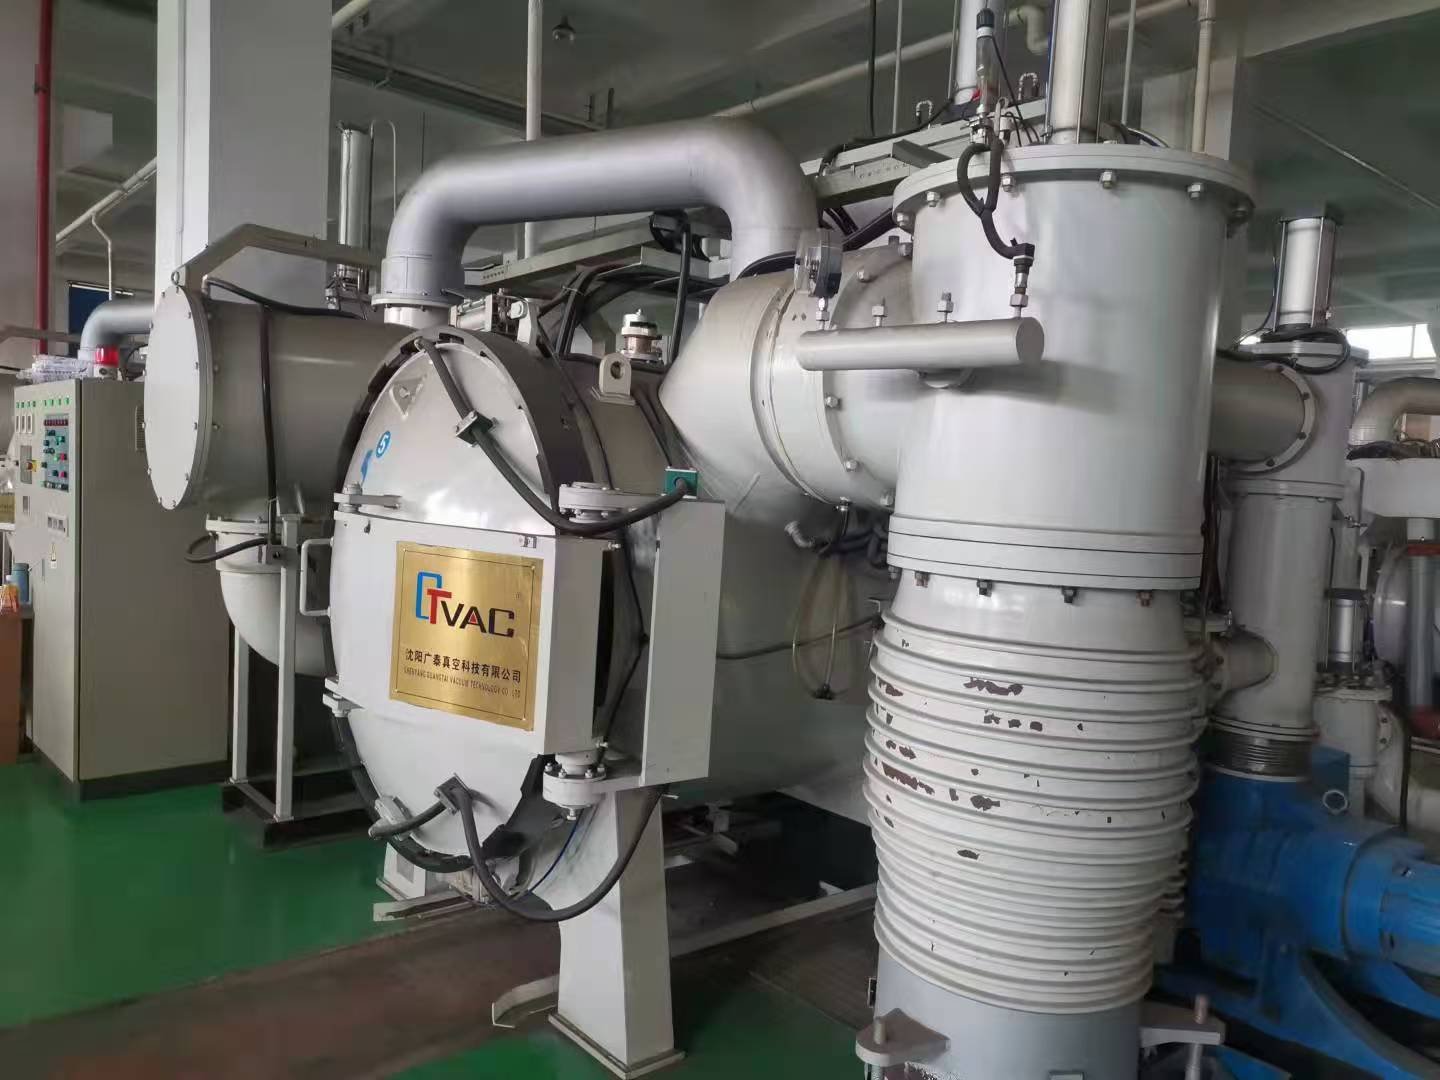
Melting, jet milling, pressing and vacuum sintering happen upstream at a partner factory. That stage fixes the magnetic properties of the material, and it is the one stage we do not cut or change. We inspect every blank when it arrives at our neodymium magnet factory, before any cutting time is spent on it.
Where to Go Next
See Production Flow for the sequence these machines run in, or Quality & Safety for the three inspection points.
Start the Conversation
Send a drawing, a 3D file or a sample. We come back with questions, a proposal or a quote, whichever helps most at that stage.